Série SHG · Portique à table fixe

Machine de découpe de grands blocs de graphite de la série SHG

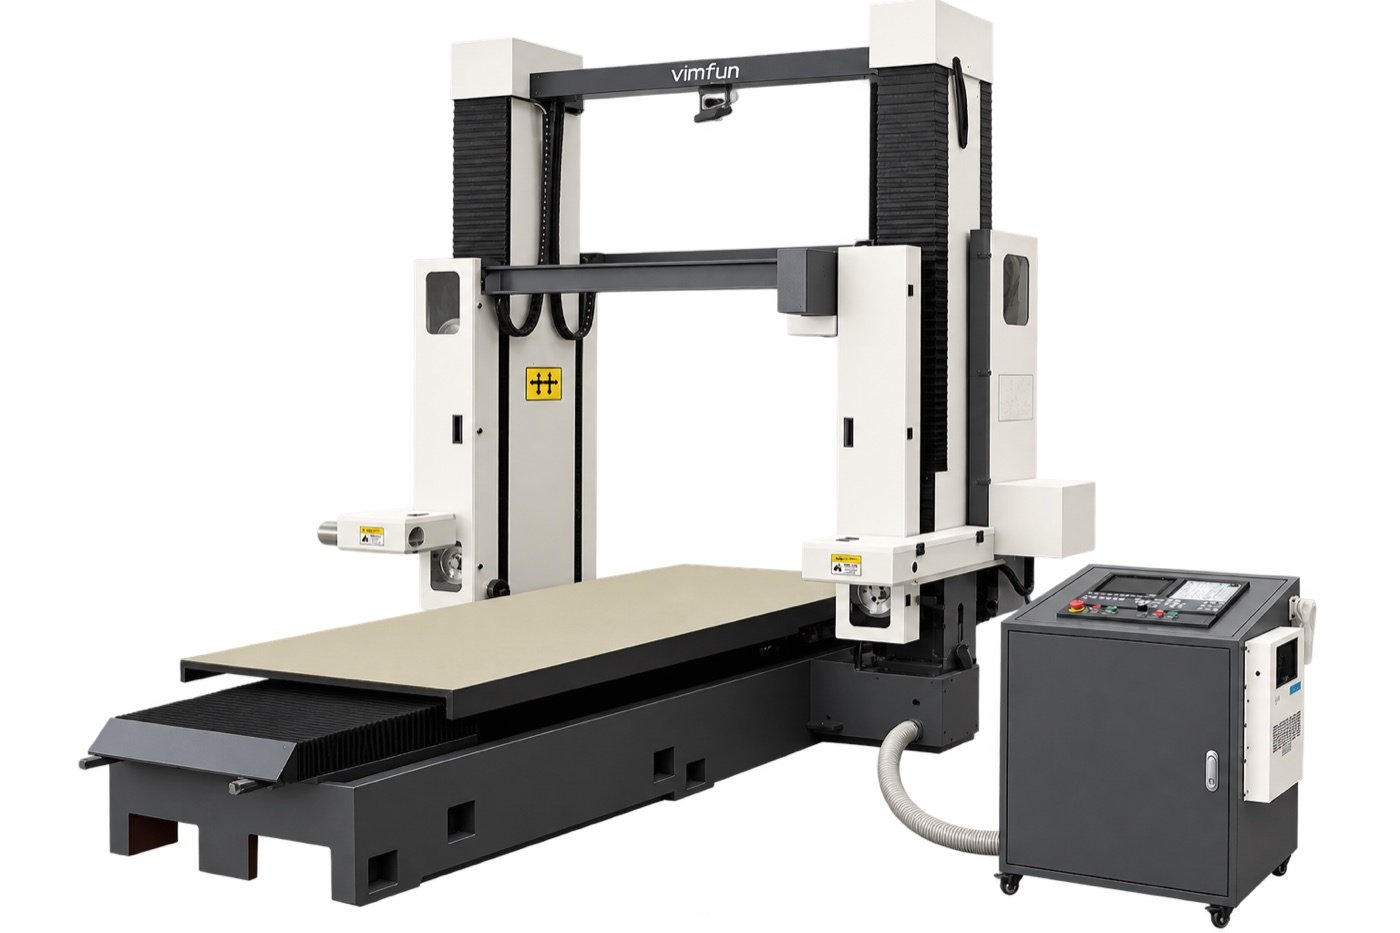
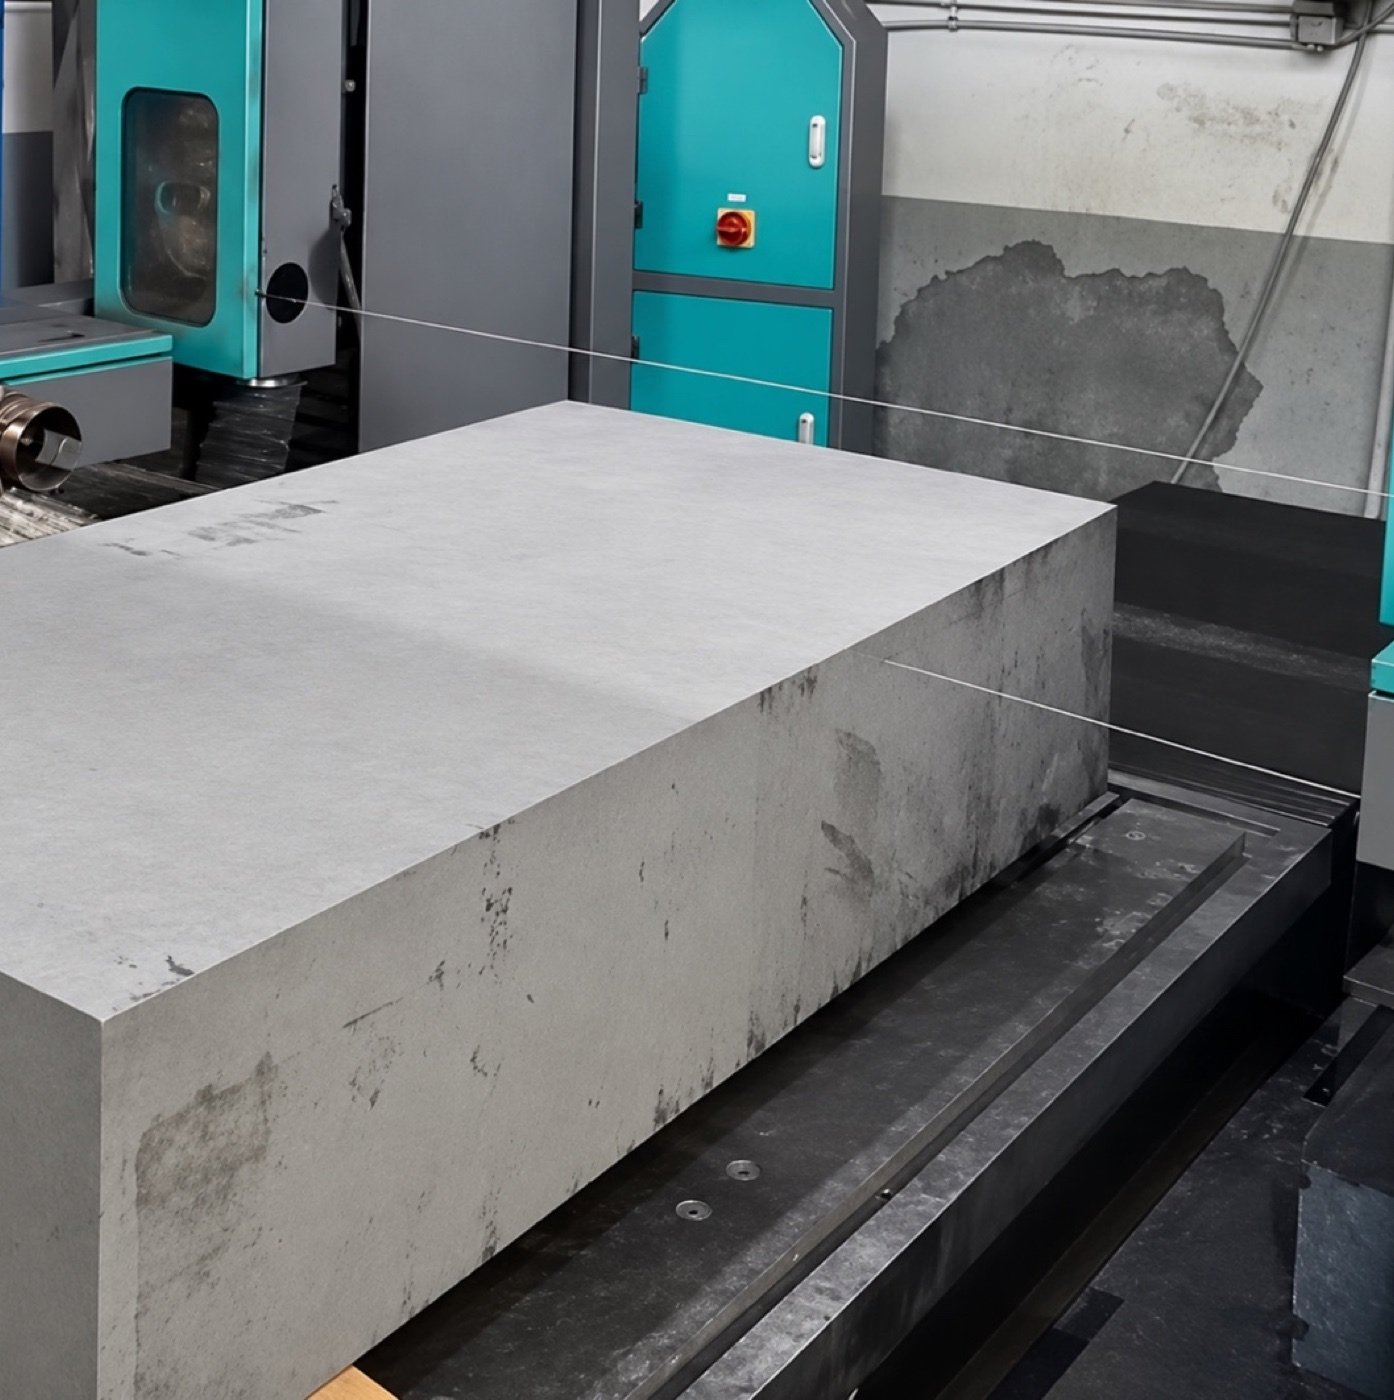
La série SHG découpe de grands blocs de graphite en dalles, plaques et ébauches profilées. Des têtes de coupe horizontales et verticales séparées se déplacent au-dessus d'une table basse stationnaire, de sorte que le bloc puisse rester dans la même configuration lors du changement de direction de coupe.

Choisissez parmi quatre modèles standard en fonction du mode de coupe requis et des dimensions complètes du bloc. La capacité standard atteint 3 300 mm en mode simple et 2 500 mm en mode combiné.

Utilisez la SHG comme machine de sciage de blocs de graphite pour des coupes droites. Comparez les enveloppes de travail pour la coupe horizontale et verticale du graphite avant de choisir un modèle.

3 300 mmlongueur en mode simple
2,500 mmlongueur en mode combiné
0–50 m/svitesse du fil de la machine
4 modèlesconfigurations standard
Demander un devis Comparer les modèles · Voir comment ça marche

Avantages clés de la série SHG

  • Table de travail fixe. Les ensembles de coupe se déplacent autour du bloc pendant que le bloc reste sur la table.
  • Deux têtes de coupe indépendantes. Sélectionnez la coupe horizontale, verticale ou combinée en fonction de la pièce.
  • Hauteur de chargement faible. Planifiez le chargement, les supports et les faces de localisation en fonction du poids et des dimensions réels du stock de graphite.
  • Profils X/Z programmés. Découpez des ébauches façonnées sur le portique après confirmation du contour et du dégagement du montage.

Regardez la série SHG en fonctionnement

La démonstration de la série Vimfun couvre trois modes de coupe dans une seule configuration. Utilisez-la pour examiner le positionnement de la pièce et le mouvement de la tête de coupe, ainsi que le tableau de capacité des modèles.

Watch on YouTube

Comparaison des modèles SHG

Vérifiez les dimensions complètes de votre bloc par rapport au mode de coupe que vous prévoyez d'utiliser. Les dimensions sont en millimètres, indiquées comme longueur × largeur × hauteur.

ModèleHorizontal uniquementVertical uniquementHorizontal + vertical combiné
SHG250-1202500 × 1200 × 10002500 × 1200 × 10001800 × 1200 × 1000
SHG280-1402800 × 1400 × 14002800 × 1400 × confirmer H2200 × 1400 × confirmer H
SHG300-1703000 × 1700 × 14003000 × 1700 × confirmer H2400 × 1400 × confirmer H
SHG330-1203300 × 1200 × 10003300 × 1200 × 10002500 × 1200 × 1000

Confirmer H signifie que la hauteur disponible nécessite une révision de la configuration. Les dimensions sont nominales et sujettes à confirmation de commande.

Spécifications techniques

SpécificationsSHG250-120SHG280-140SHG300-170SHG330-120
Course X / Y / Z (mm)2500 / 1000 / 10002800 / 1400 / 14003000 / 1400 / 14003300 / 1000 / 1000
Table de travail (mm)2500 × 10002800 × 10003000 × 10003300 × 1000
Machine weight, approx. (kg)4200450046504400
Overall dimensions, approx. (m)3.9 × 2.3 × 2.454.2 × 2.45 × 2.54.2 × 2.8 × 2.54.5 × 2.8 × 2.5

Standard supply is AC 380 V, three-phase. Installed power is approximately 9 kW. Machine weights exclude packing. Confirm workpiece support and table load for your block.

How the SHG Fixed-Table Gantry Works

The SHG holds the graphite block stationary on a low table. Two independent cutting assemblies move on the gantry, each with its own closed-loop cutting wire. The numbers in the schematic match the component list below.

SHG fixed-table gantry: numbered components and X, Y, Z motion A fixed gantry beam spans the width of a stationary graphite block on a low worktable. Numbers 1 to 5 mark the gantry beam, horizontal cutting unit, vertical cutting unit, graphite workpiece and worktable. Y runs left to right along the beam across the block width, X runs front to back along the block length, and Z is vertical. Y · across block widthZX · along block length Fixed gantry beam Vertical cutting unit Graphite workpiece 134 Horizontal cutting unitFixed worktable 25 YXZ Blue dashed lines: closed-loop cutting wires
Functional schematic. Component positions, wire routing and distances are simplified and not to scale.
  1. Fixed gantry beam. The cross-beam spans the block width (Y direction) and carries and guides the cutting assemblies over the block.
  2. Horizontal cutting unit. The first assembly, with its own closed-loop wire.
  3. Vertical cutting unit. A second, independent assembly with its own wire for the other cutting direction.
  4. Graphite workpiece. The block stays located on the table while the cutting assemblies move around it.
  5. Table de travail fixe. A low, stationary table supports the block and its fixtures. Confirm support and table load for the actual stock.

X, Y and Z motion

AxisArrow in schematicWhat movesFonction
XFront to back, along the block lengthCutting assemblies travel front to back along the block length; both units share this longitudinal travel.Squaring, trimming and long straight cuts.
YLeft to right, across the block width (along the beam)Cutting assemblies move across the width of the workpiece.Positionnement de la coupe sur la largeur du bloc.
ZVerticaleDéplacement vertical de l'ensemble de coupe.Alimentation de haut en bas pour le débitage et la séparation des sections.
X + ZMouvement coordonnéLes deux axes se déplacent en même temps sous le contrôle de la CNC.Programmed contour cuts for shaped blanks.

How X and Z work together on a contour

X/Z interpolation along a programmed contour A curved programmed profile crosses a graphite block outline. At one point the cutting path is split into a horizontal X component and a vertical Z component that are moved together. Finished blank Déchets ΔXΔZ XZ Side view, X/Z planeProgrammed profile (illustrative)
Illustrative profile only. Not a real part drawing.
  1. Position. Set the cut position across the block with Y.
  2. Program the profile. The contour is defined in the X/Z plane.
  3. Interpolate. The controller moves X and Z together. At every point on the profile, the ratio of ΔX to ΔZ sets the local cutting direction.
  4. Follow the path. The resultant motion traces the programmed shape through the graphite, so one pass produces a curved or stepped edge instead of a straight cut.

Share the profile drawing so Vimfun can confirm feasibility and fixture clearance.

Wire speed and feed rate are different

Vitesse du fil

m/s. How fast the closed-loop wire circulates around its loop. It is set by the wire drive.

Machine range: 0–50 m/s. Initial window for isostatic and fine-grain graphite: 30–40 m/s.

Vitesse d'alimentation

mm/min. How fast CNC motion advances the cutting assembly relative to the block, which is how fast the cut progresses through the graphite.

Machine range: X 0.01–3000 mm/min; Y and Z 0.01–5000 mm/min. Initial window for isostatic and fine-grain graphite: 50–100 mm/min.

Why the two numbers are not interchangeable

Wire speed is the motion of the cutting tool itself. Feed rate is the motion of the axes. At the initial window, the wire travels roughly 18,000 to 48,000 times farther per minute than the head advances. Raising wire speed does not advance the cut, and raising feed does not make the wire run faster. Set both during commissioning for the actual grade and section size.

Why combined cutting shortens the workable length

Single-mode length matches the X travel of the model. When the horizontal and vertical units work in the same setup, both assemblies share the same X stroke instead of each having the full stroke. The block must therefore fit a shorter envelope. On the standard models, the combined-mode length is 600 to 800 mm below the single-mode length.

Single-mode and combined-mode block length by SHG model Paired bars compare the single-mode block length with the shorter combined-mode block length for each SHG model, in millimetres. 01,0002,0003,000SHG250-1202,5001,800 (−700)SHG280-1402,8002,200 (−600)SHG300-1703,0002,400 (−600)SHG330-1203,3002,500 (−800) Single mode, mm Combined horizontal + vertical, mm (reduction)
Nominal lengths from the model comparison table. Subject to order confirmation.
Example selection

A 2,400 × 1,400 × 1,200 mm block requiring both directions puts the SHG300-170 on the shortlist. Its combined-mode length and width match the nominal block size. Confirm usable height, actual stock dimensions and support clearance before selecting it. The SHG330-120 has a 1,200 mm combined-mode width, so this block exceeds its width limit.

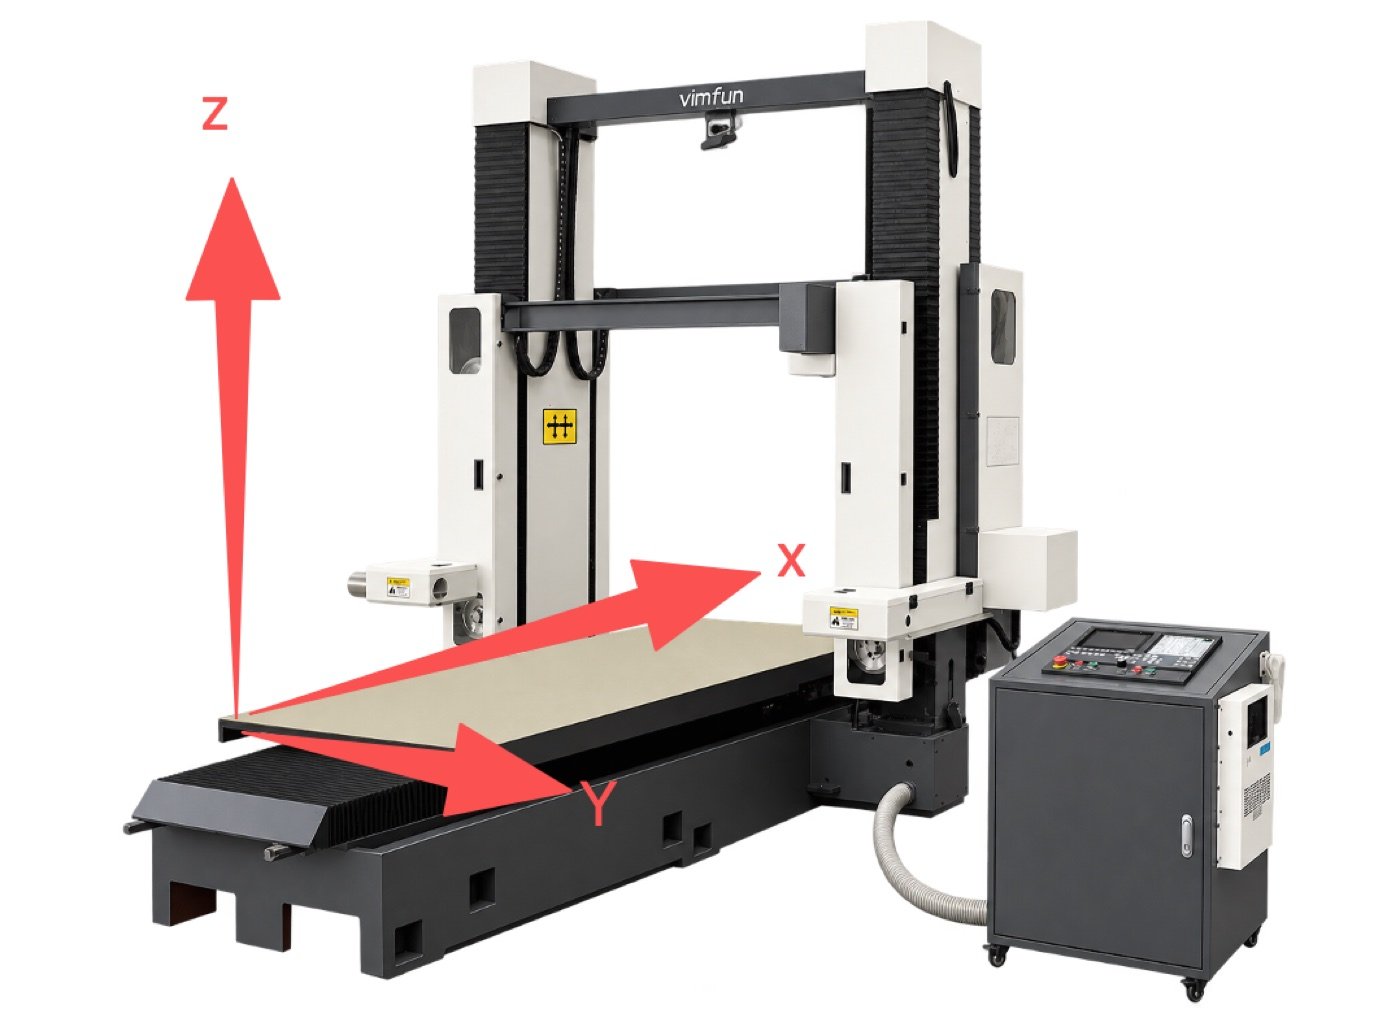
SHG gantry overview with X, Y and Z direction arrows
X, Y and Z axis illustration

Workpiece setup

Locate the block from a stable datum, check support under the cut-off section, and allow space for dust extraction and handling before the first pass.

Cutting operations

Slab and plate cutting

Feed the cutting head down through the block to separate slabs or part off sections.

Block squaring and trimming

Cut along the block length to trim edges and prepare stock for downstream machining.

Contour cutting

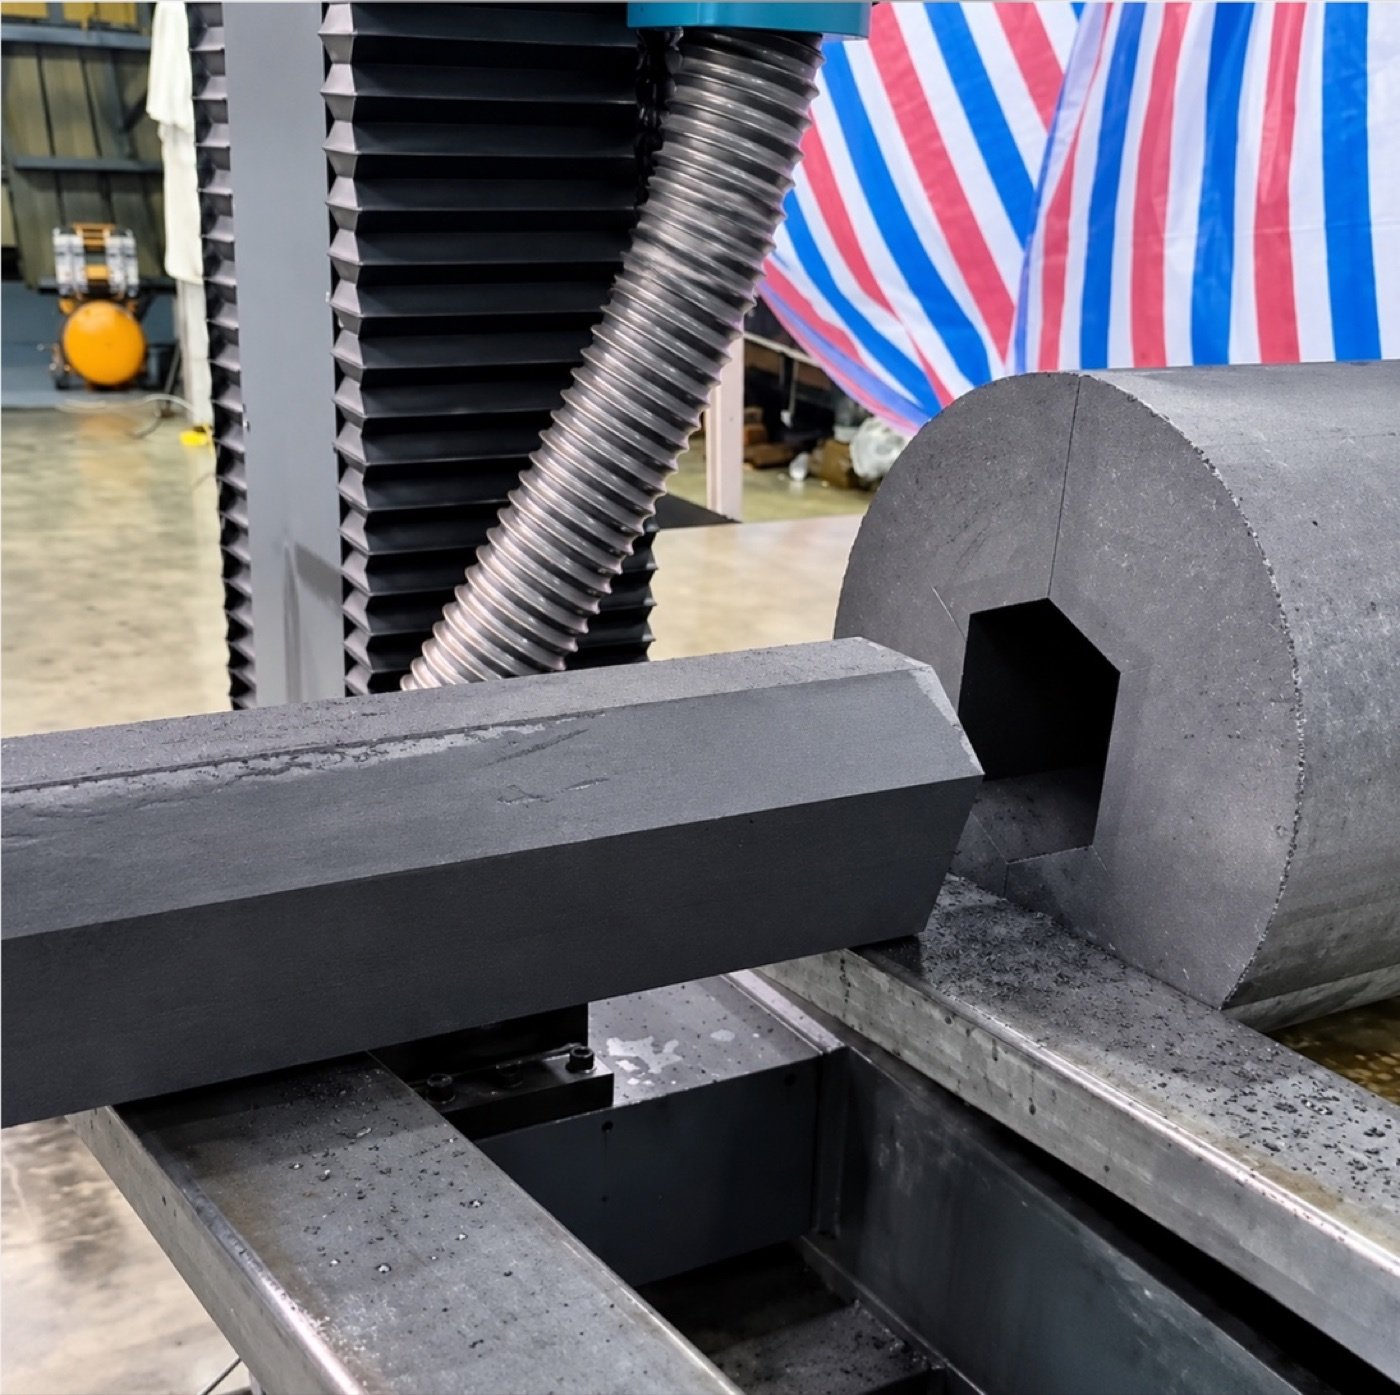
Use coordinated X/Z motion to cut a programmed profile for shaped graphite blanks.

Cut Sample and Acceptance Checks

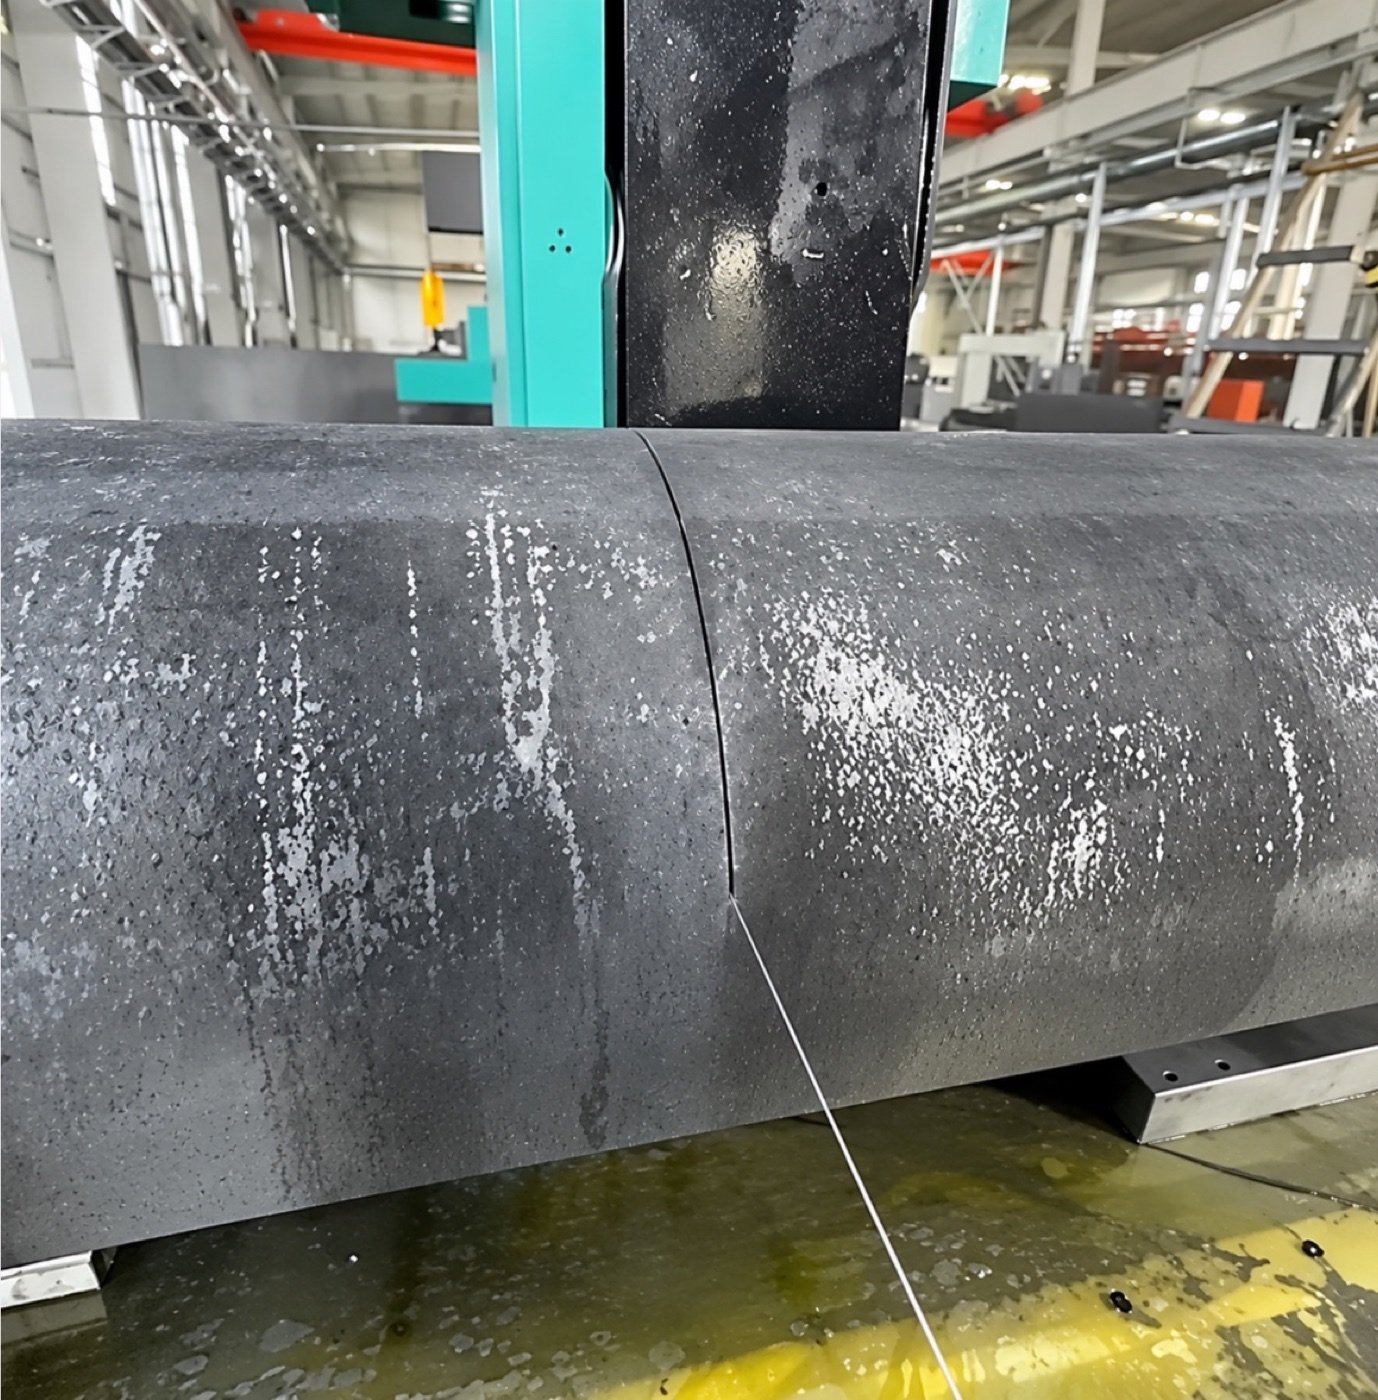
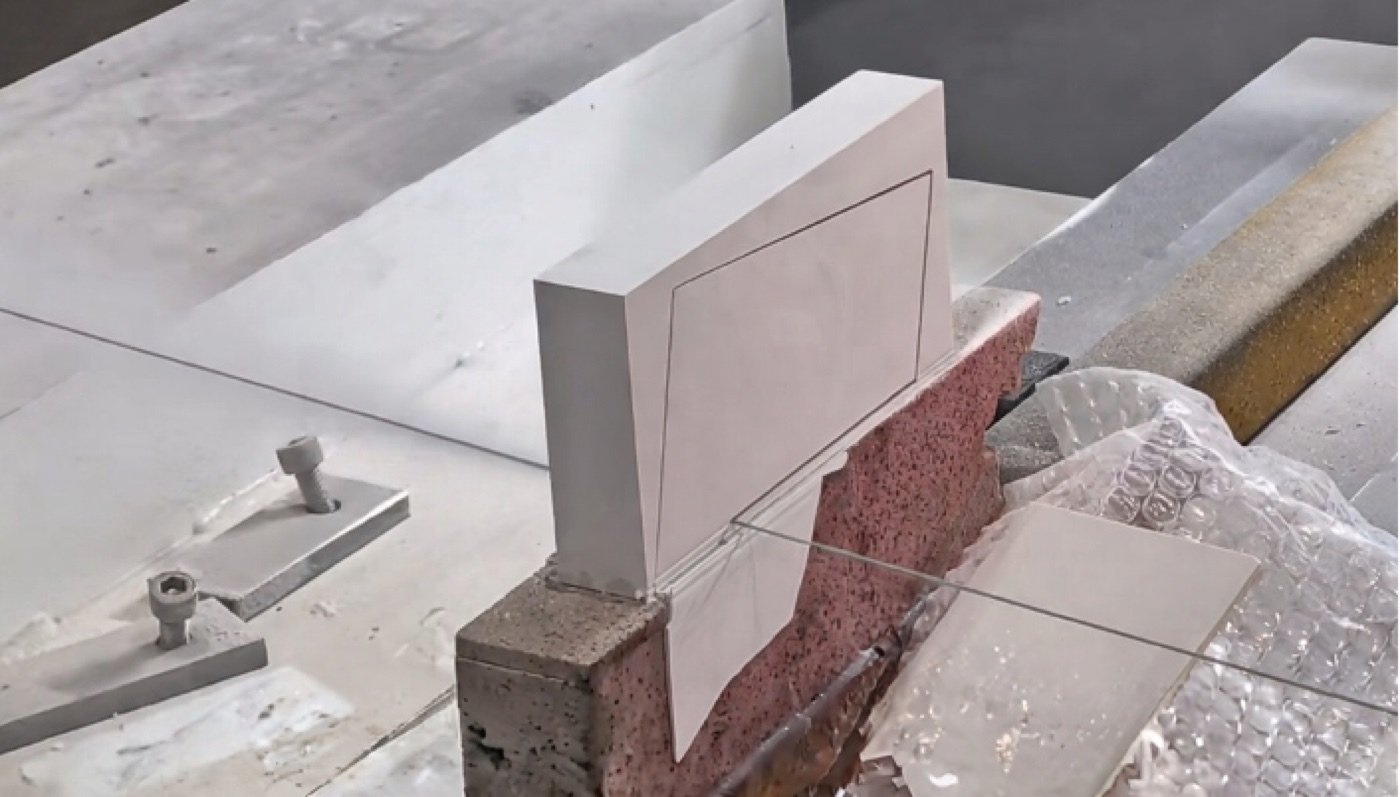
Cut sample clamped on a work surface
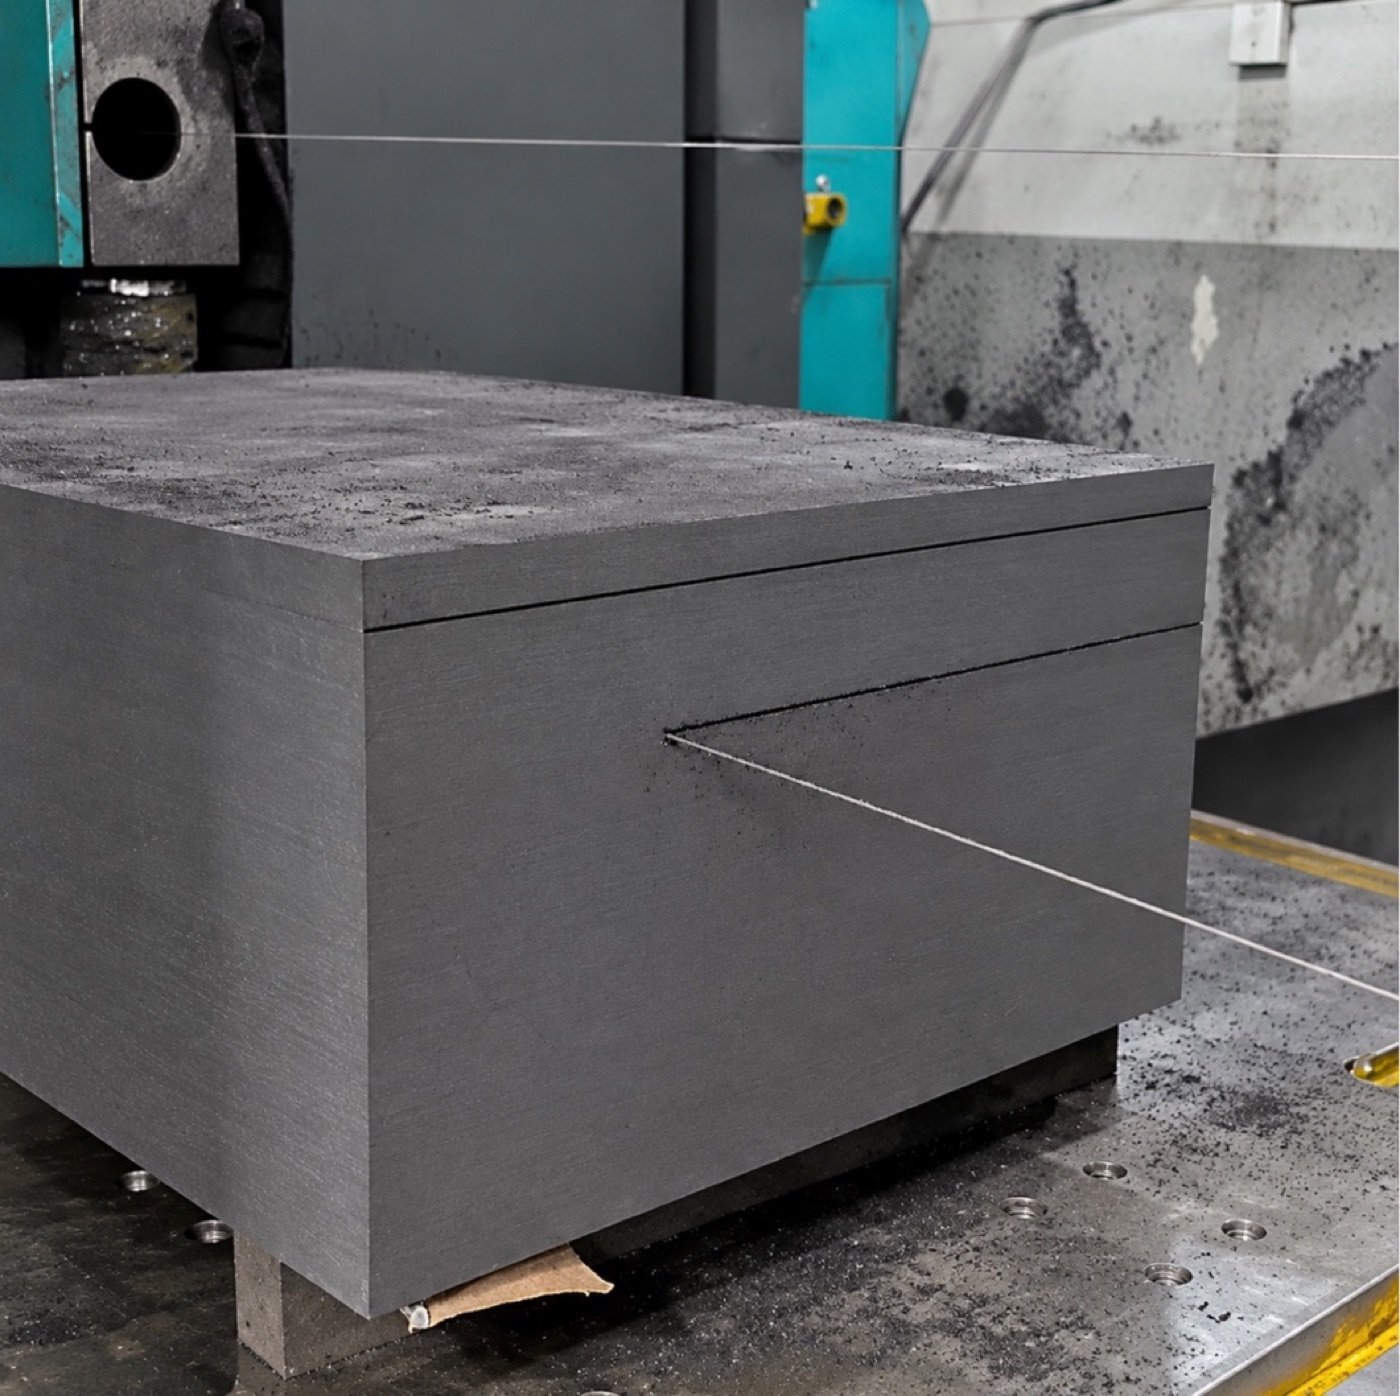
Additional sample view from the equipment document

What to verify during a trial cut

Agree on the finished blank dimensions and machining allowance before selecting feed or cutting direction. Inspect the reference face, edge condition and dimensional variation at agreed positions. Record graphite grade, cut orientation and support to make the result repeatable.

Graphite cutting setup

Typical materials include isostatic, extruded and fine-grain graphite. The SHG series cuts graphite dry. Plan dust extraction at the cutting zone and confirm workpiece support and fixturing for your block dimensions.

For isostatic and fine-grain graphite, the initial process window is 30–40 m/s wire speed and 50–100 mm/min feed. Initial wire diameter and tension ranges are 0.6–1.0 mm and 150–200 N. The machine wire speed range is 0–50 m/s. Set production parameters during commissioning for the actual grade and section size.

Frequently asked questions

Which model fits a 3.3 m graphite block?

The SHG330-120 accommodates a block up to 3,300 mm long in either single cutting mode, with a nominal envelope of 3,300 × 1,200 × 1,000 mm. Its combined-mode length limit is 2,500 mm.

Can the same block be cut horizontally and vertically?

Yes. The separate cutting units are mounted on one frame. Check the combined-mode envelope for the selected model before committing to the cut plan.

Can the machine cut profiled graphite blanks?

Coordinated X/Z interpolation supports programmed contour cuts. Share the profile drawing to confirm feasibility.

Does graphite cutting require coolant?

The SHG graphite process is dry. Provide dust extraction at the cutting zone.

Can Vimfun build a machine for a different block size?

X, Y and Z travel, worktable dimensions, fixturing and dust extraction interfaces can be specified to suit the installation.

Request an SHG configuration and quote

Workpiece and output

  • Graphite grade and max. block size (L × W × H)
  • Block weight and loading method
  • Cutting directions, part drawing and output per shift

Installation

  • Power supply and floor space
  • Dust collection and extraction connection

Discuss your SHG configuration

Request an SHG quote
Défiler vers le haut