SHG Series · Fixed-table gantry

SHG Series Large Graphite Block Cutting Machine

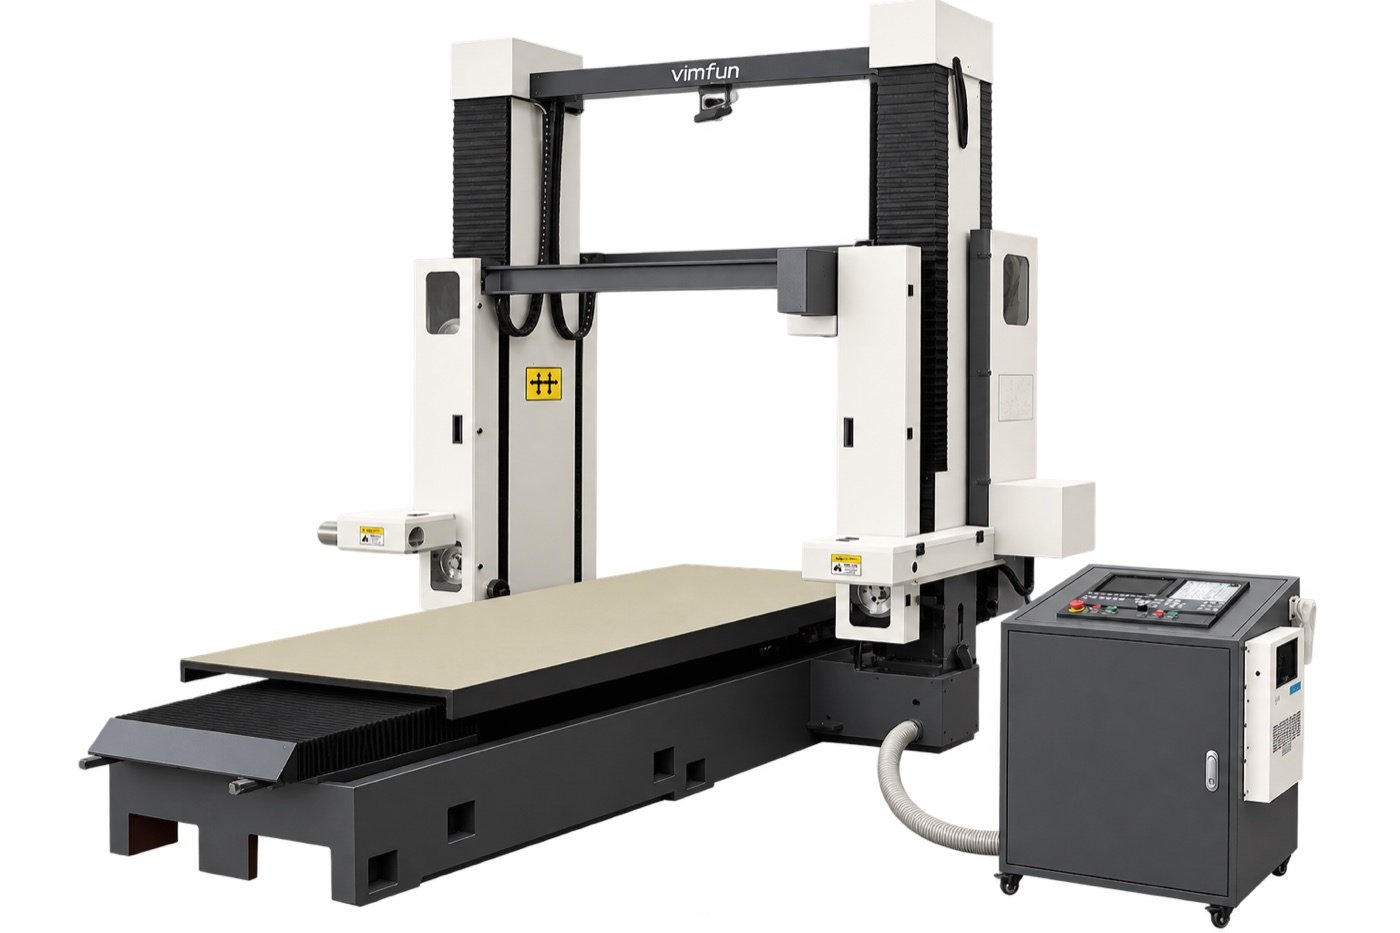
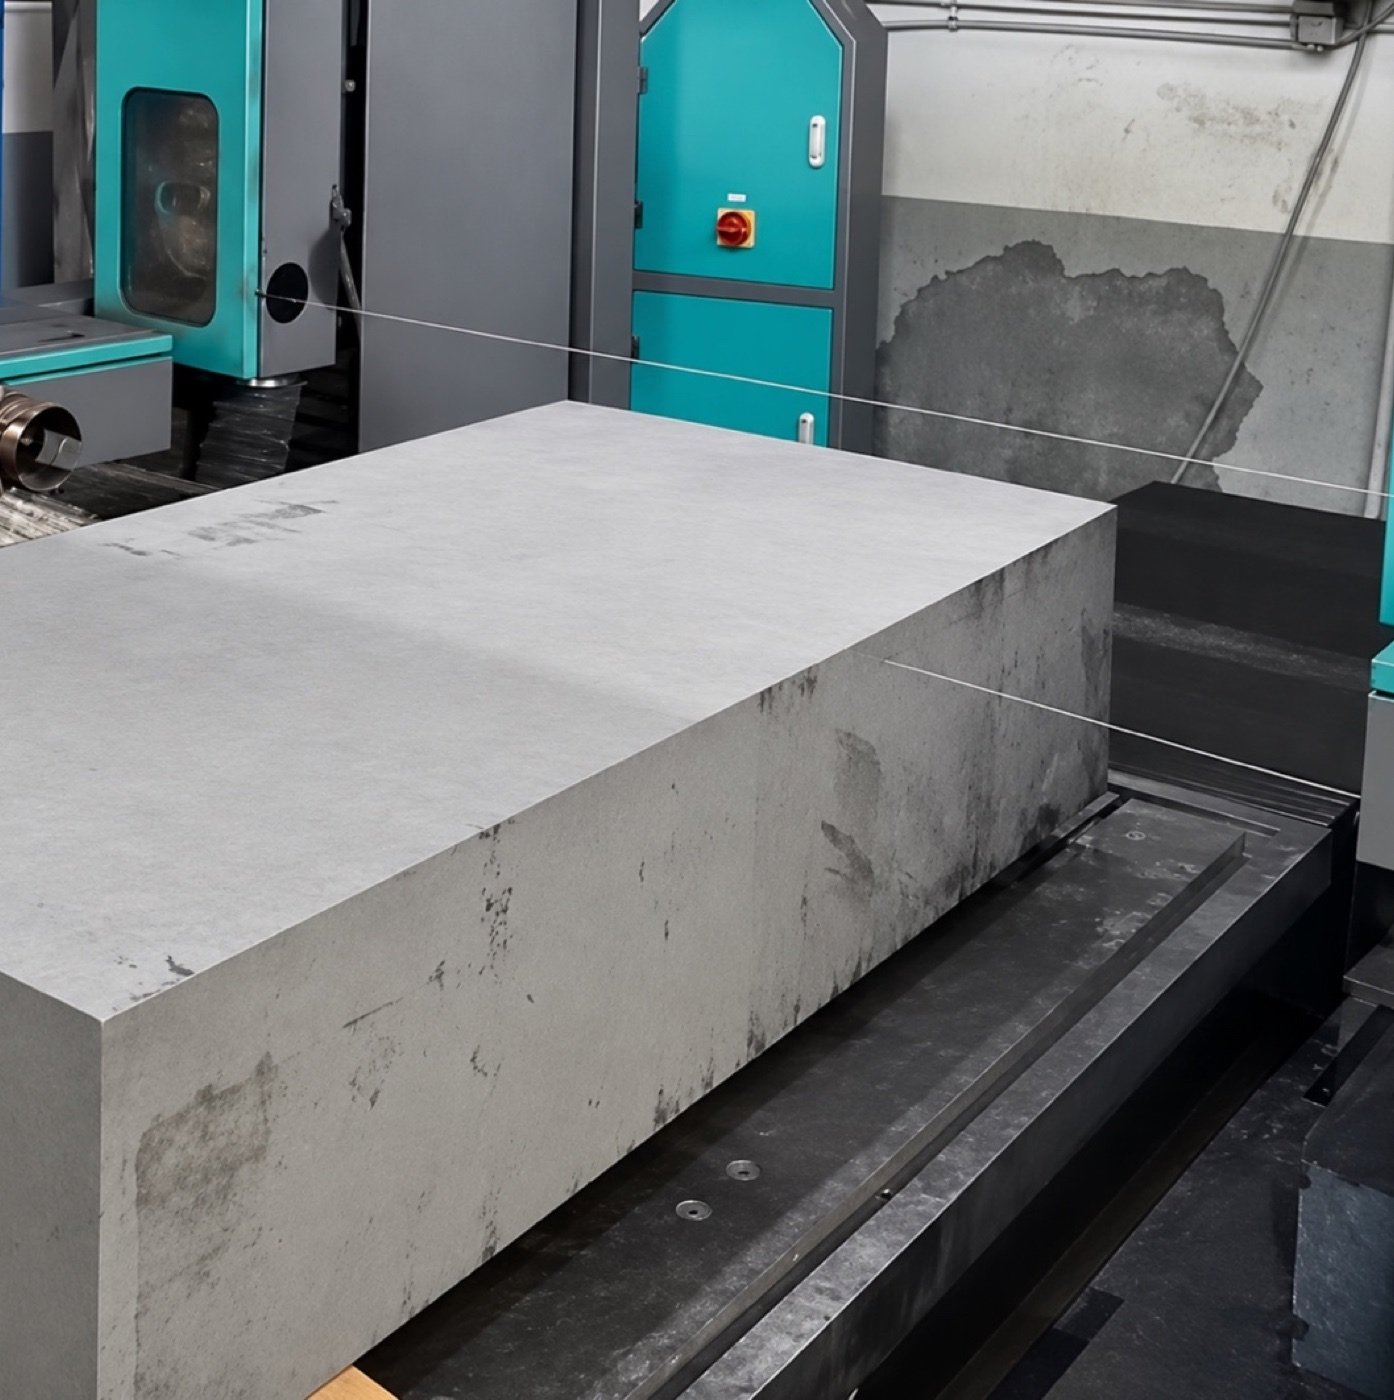
The SHG series cuts large graphite blocks into slabs, plates and profiled blanks. Separate horizontal and vertical cutting heads travel above a low, stationary table, so the block can stay in the same setup when switching cutting directions.

Choose from four standard models by the required cutting mode and full block dimensions. Standard capacity reaches 3,300 mm in a single mode and 2,500 mm in combined mode.

Use the SHG as a graphite block slabbing machine for straight cuts. Compare the working envelopes for horizontal and vertical graphite cutting before choosing a model.

3,300 mmsingle-mode length
2,500 mmcombined-mode length
0–50 m/smachine wire speed
4 modelsstandard configurations
Get a quote Compare models · See how it works

Key Advantages of the SHG Series

  • Fixed worktable. The cutting assemblies move around the block while the block stays on the table.
  • Two independent cutting heads. Select horizontal, vertical or combined cutting according to the workpiece.
  • Low loading height. Plan loading, supports and locating faces around the actual weight and dimensions of the graphite stock.
  • Programmed X/Z profiles. Cut shaped blanks on the gantry after confirming the contour and fixture clearance.

Watch the SHG series in operation

Vimfun’s series demonstration covers three cutting modes in one setup. Use it to review workpiece positioning and cutting-head movement alongside the model capacity table.

Watch on YouTube

SHG model comparison

Check your full block dimensions against the cutting mode you plan to use. Dimensions are in millimetres, listed as length × width × height.

モデルHorizontal onlyVertical onlyCombined horizontal + vertical
SHG250-1202500 × 1200 × 10002500 × 1200 × 10001800 × 1200 × 1000
SHG280-1402800 × 1400 × 14002800 × 1400 × confirm H2200 × 1400 × confirm H
SHG300-1703000 × 1700 × 14003000 × 1700 × confirm H2400 × 1400 × confirm H
SHG330-1203300 × 1200 × 10003300 × 1200 × 10002500 × 1200 × 1000

Confirm H means the available height needs configuration review. Dimensions are nominal and subject to order confirmation.

Technical specifications

仕様SHG250-120SHG280-140SHG300-170SHG330-120
X / Y / Z travel (mm)2500 / 1000 / 10002800 / 1400 / 14003000 / 1400 / 14003300 / 1000 / 1000
Worktable (mm)2500 × 10002800 × 10003000 × 10003300 × 1000
Machine weight, approx. (kg)4200450046504400
Overall dimensions, approx. (m)3.9 × 2.3 × 2.454.2 × 2.45 × 2.54.2 × 2.8 × 2.54.5 × 2.8 × 2.5

Standard supply is AC 380 V, three-phase. Installed power is approximately 9 kW. Machine weights exclude packing. Confirm workpiece support and table load for your block.

How the SHG Fixed-Table Gantry Works

The SHG holds the graphite block stationary on a low table. Two independent cutting assemblies move on the gantry, each with its own closed-loop cutting wire. The numbers in the schematic match the component list below.

SHG固定テーブルガントリー:番号付きコンポーネントとX、Y、Zモーション A fixed gantry beam spans the width of a stationary graphite block on a low worktable. Numbers 1 to 5 mark the gantry beam, horizontal cutting unit, vertical cutting unit, graphite workpiece and worktable. Y runs left to right along the beam across the block width, X runs front to back along the block length, and Z is vertical. Y · across block widthZX · along block length Fixed gantry beam Vertical cutting unit Graphite workpiece 134 Horizontal cutting unitFixed worktable 25 YXZ Blue dashed lines: closed-loop cutting wires
Functional schematic. Component positions, wire routing and distances are simplified and not to scale.
  1. Fixed gantry beam. The cross-beam spans the block width (Y direction) and carries and guides the cutting assemblies over the block.
  2. Horizontal cutting unit. The first assembly, with its own closed-loop wire.
  3. Vertical cutting unit. A second, independent assembly with its own wire for the other cutting direction.
  4. Graphite workpiece. The block stays located on the table while the cutting assemblies move around it.
  5. Fixed worktable. A low, stationary table supports the block and its fixtures. Confirm support and table load for the actual stock.

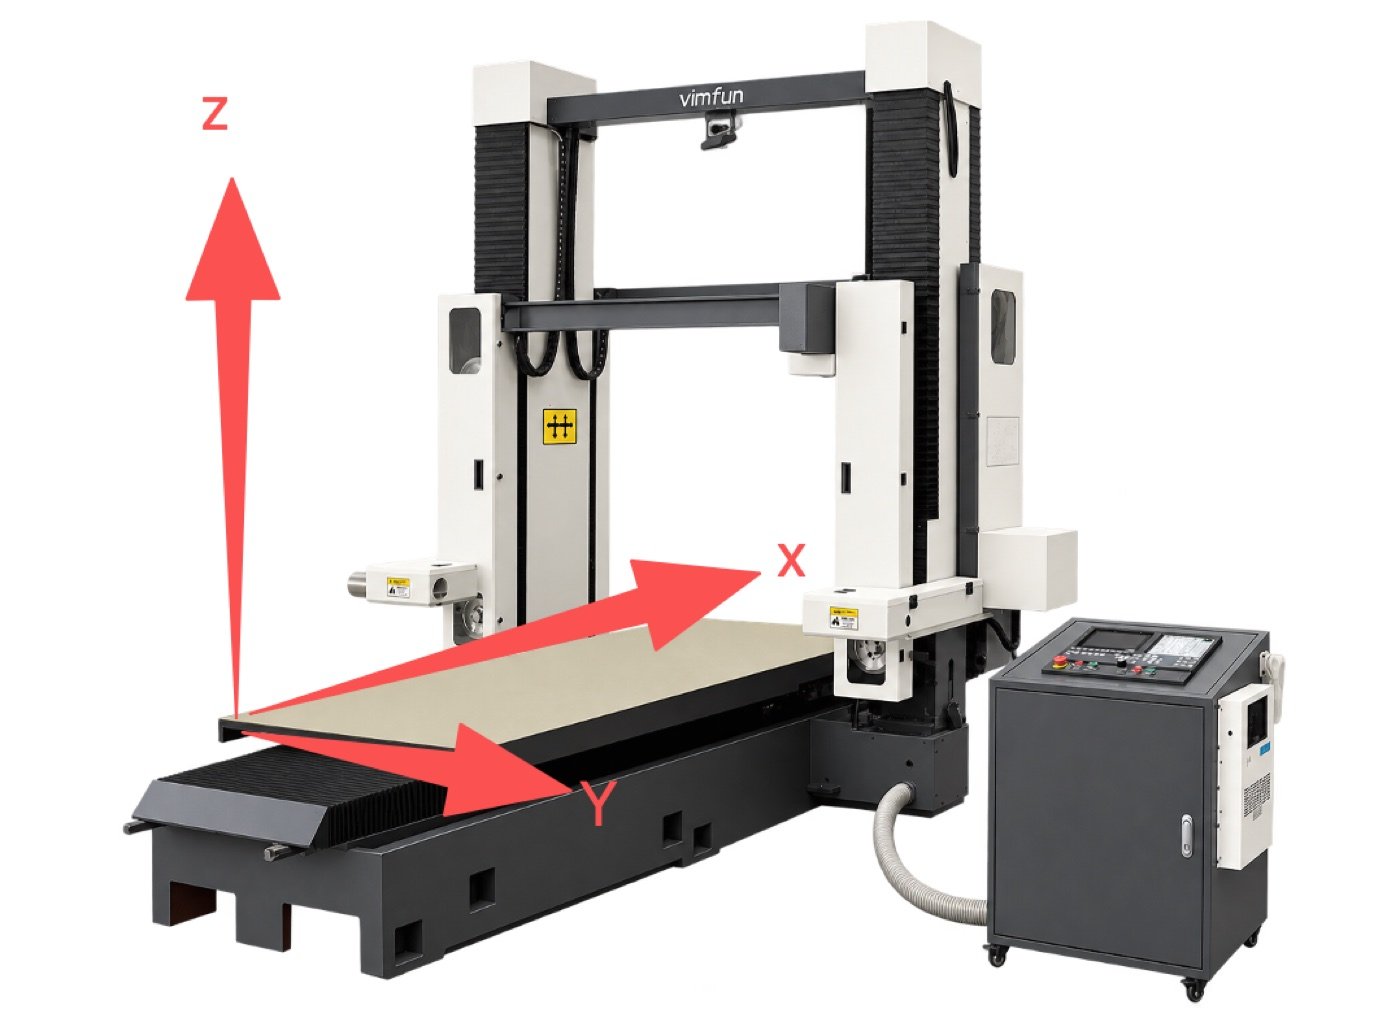
X, Y and Z motion

AxisArrow in schematicWhat moves機能
XFront to back, along the block lengthCutting assemblies travel front to back along the block length; both units share this longitudinal travel.Squaring, trimming and long straight cuts.
YLeft to right, across the block width (along the beam)Cutting assemblies move across the width of the workpiece.Positioning the cut across the width of the block.
Z縦型Vertical travel of the cutting assembly.Top-down feed for slabbing and separating sections.
X + ZCoordinated motionBoth axes move at the same time under CNC control.Programmed contour cuts for shaped blanks.

How X and Z work together on a contour

プログラムされた輪郭に沿ったX/Z補間 A curved programmed profile crosses a graphite block outline. At one point the cutting path is split into a horizontal X component and a vertical Z component that are moved together. Finished blank 無駄 ΔXΔZ XZ Side view, X/Z planeProgrammed profile (illustrative)
Illustrative profile only. Not a real part drawing.
  1. Position. Set the cut position across the block with Y.
  2. Program the profile. The contour is defined in the X/Z plane.
  3. Interpolate. The controller moves X and Z together. At every point on the profile, the ratio of ΔX to ΔZ sets the local cutting direction.
  4. Follow the path. The resultant motion traces the programmed shape through the graphite, so one pass produces a curved or stepped edge instead of a straight cut.

Share the profile drawing so Vimfun can confirm feasibility and fixture clearance.

Wire speed and feed rate are different

ワイヤースピード

m/s. How fast the closed-loop wire circulates around its loop. It is set by the wire drive.

Machine range: 0–50 m/s. Initial window for isostatic and fine-grain graphite: 30–40 m/s.

送り速度

mm/min. How fast CNC motion advances the cutting assembly relative to the block, which is how fast the cut progresses through the graphite.

Machine range: X 0.01–3000 mm/min; Y and Z 0.01–5000 mm/min. Initial window for isostatic and fine-grain graphite: 50–100 mm/min.

Why the two numbers are not interchangeable

Wire speed is the motion of the cutting tool itself. Feed rate is the motion of the axes. At the initial window, the wire travels roughly 18,000 to 48,000 times farther per minute than the head advances. Raising wire speed does not advance the cut, and raising feed does not make the wire run faster. Set both during commissioning for the actual grade and section size.

Why combined cutting shortens the workable length

Single-mode length matches the X travel of the model. When the horizontal and vertical units work in the same setup, both assemblies share the same X stroke instead of each having the full stroke. The block must therefore fit a shorter envelope. On the standard models, the combined-mode length is 600 to 800 mm below the single-mode length.

SHGモデル別の単一モードおよび複合モードブロック長 Paired bars compare the single-mode block length with the shorter combined-mode block length for each SHG model, in millimetres. 01,0002,0003,000SHG250-1202,5001,800 (−700)SHG280-1402,8002,200 (−600)SHG300-1703,0002,400 (−600)SHG330-1203,3002,500 (−800) Single mode, mm Combined horizontal + vertical, mm (reduction)
Nominal lengths from the model comparison table. Subject to order confirmation.
Example selection

A 2,400 × 1,400 × 1,200 mm block requiring both directions puts the SHG300-170 on the shortlist. Its combined-mode length and width match the nominal block size. Confirm usable height, actual stock dimensions and support clearance before selecting it. The SHG330-120 has a 1,200 mm combined-mode width, so this block exceeds its width limit.

X、Y、Z方向矢印付きSHGガントリー概要
X, Y and Z axis illustration

Workpiece setup

Locate the block from a stable datum, check support under the cut-off section, and allow space for dust extraction and handling before the first pass.

Cutting operations

Slab and plate cutting

Feed the cutting head down through the block to separate slabs or part off sections.

Block squaring and trimming

Cut along the block length to trim edges and prepare stock for downstream machining.

Contour cutting

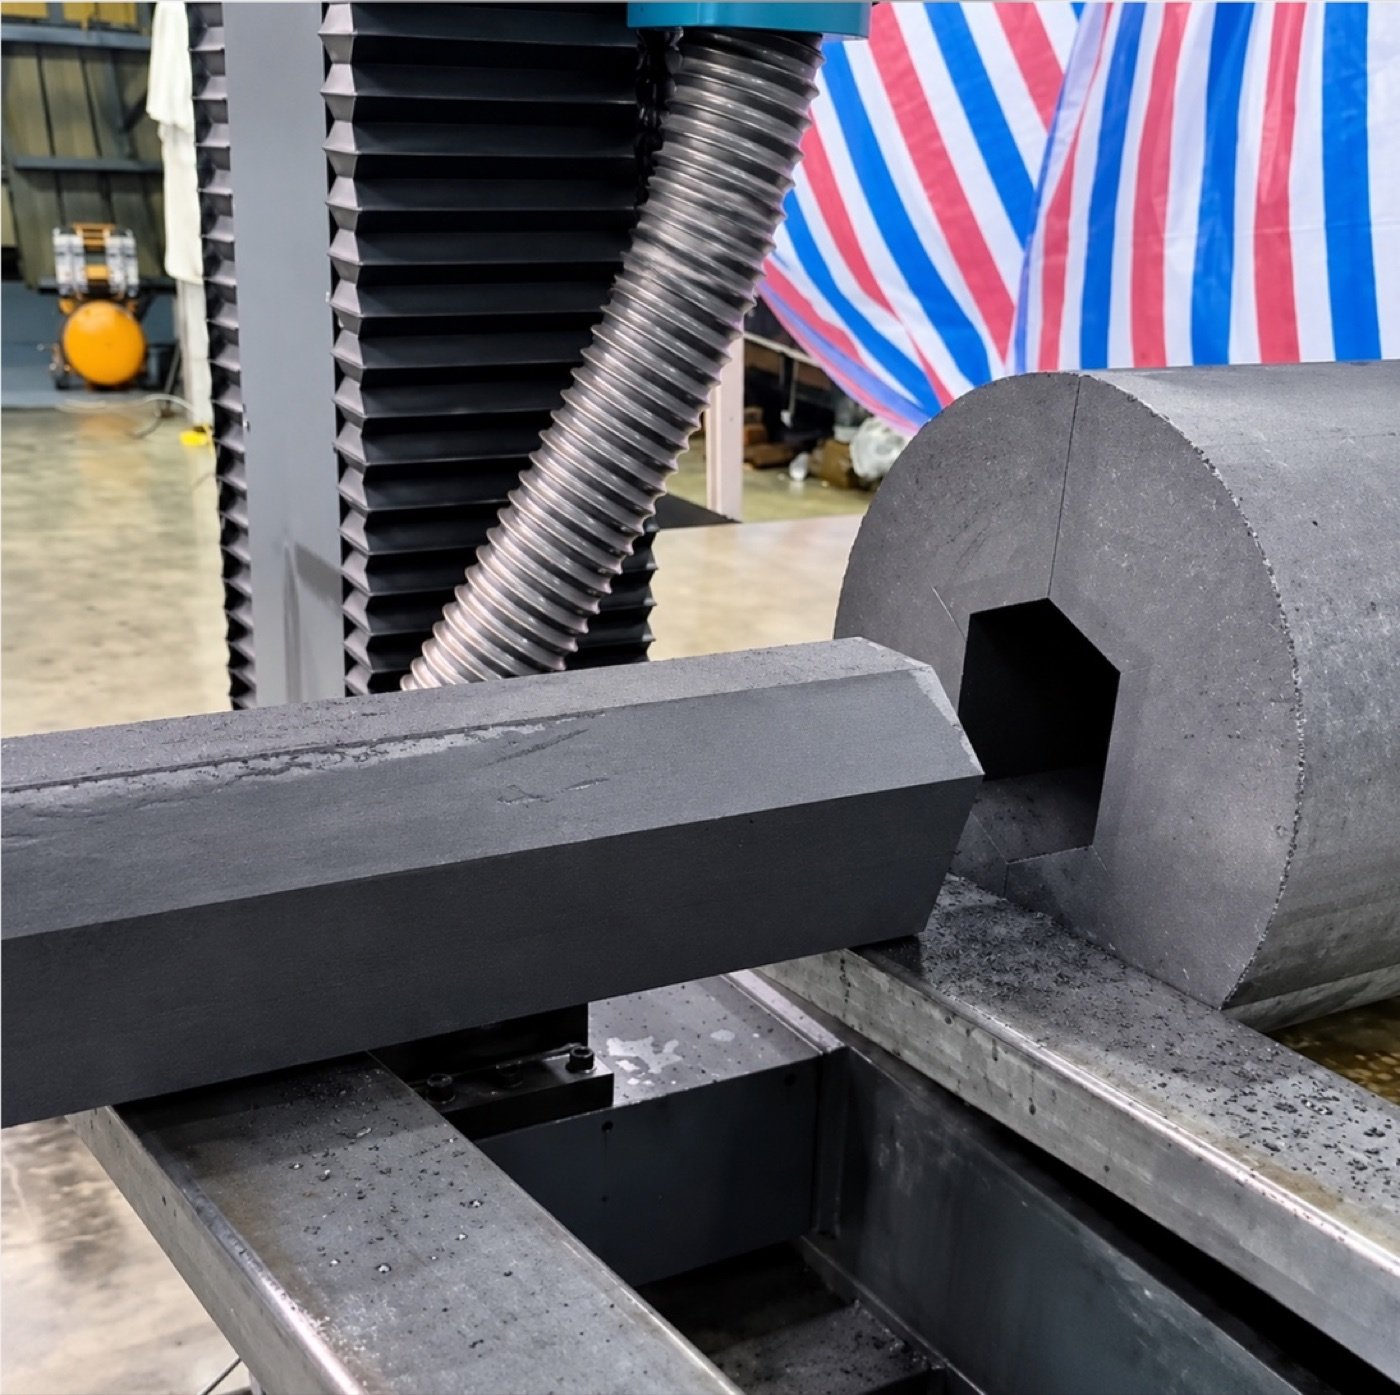
Use coordinated X/Z motion to cut a programmed profile for shaped graphite blanks.

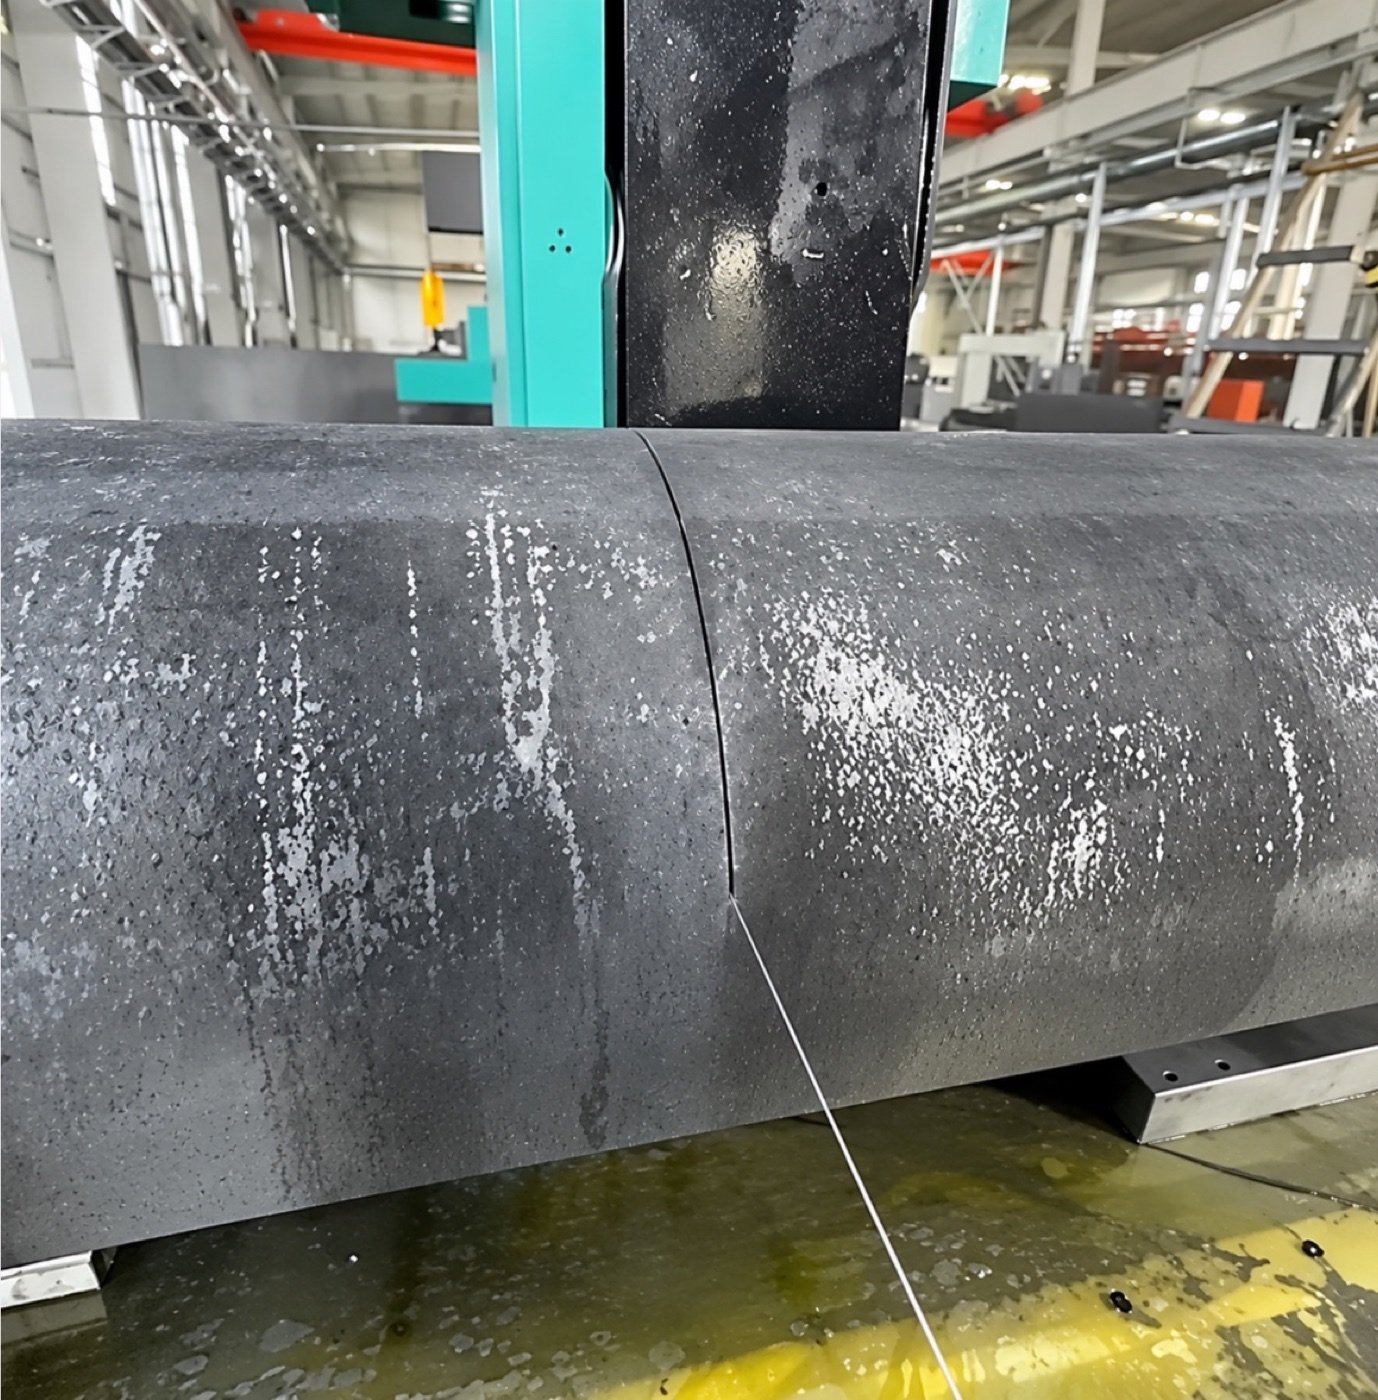
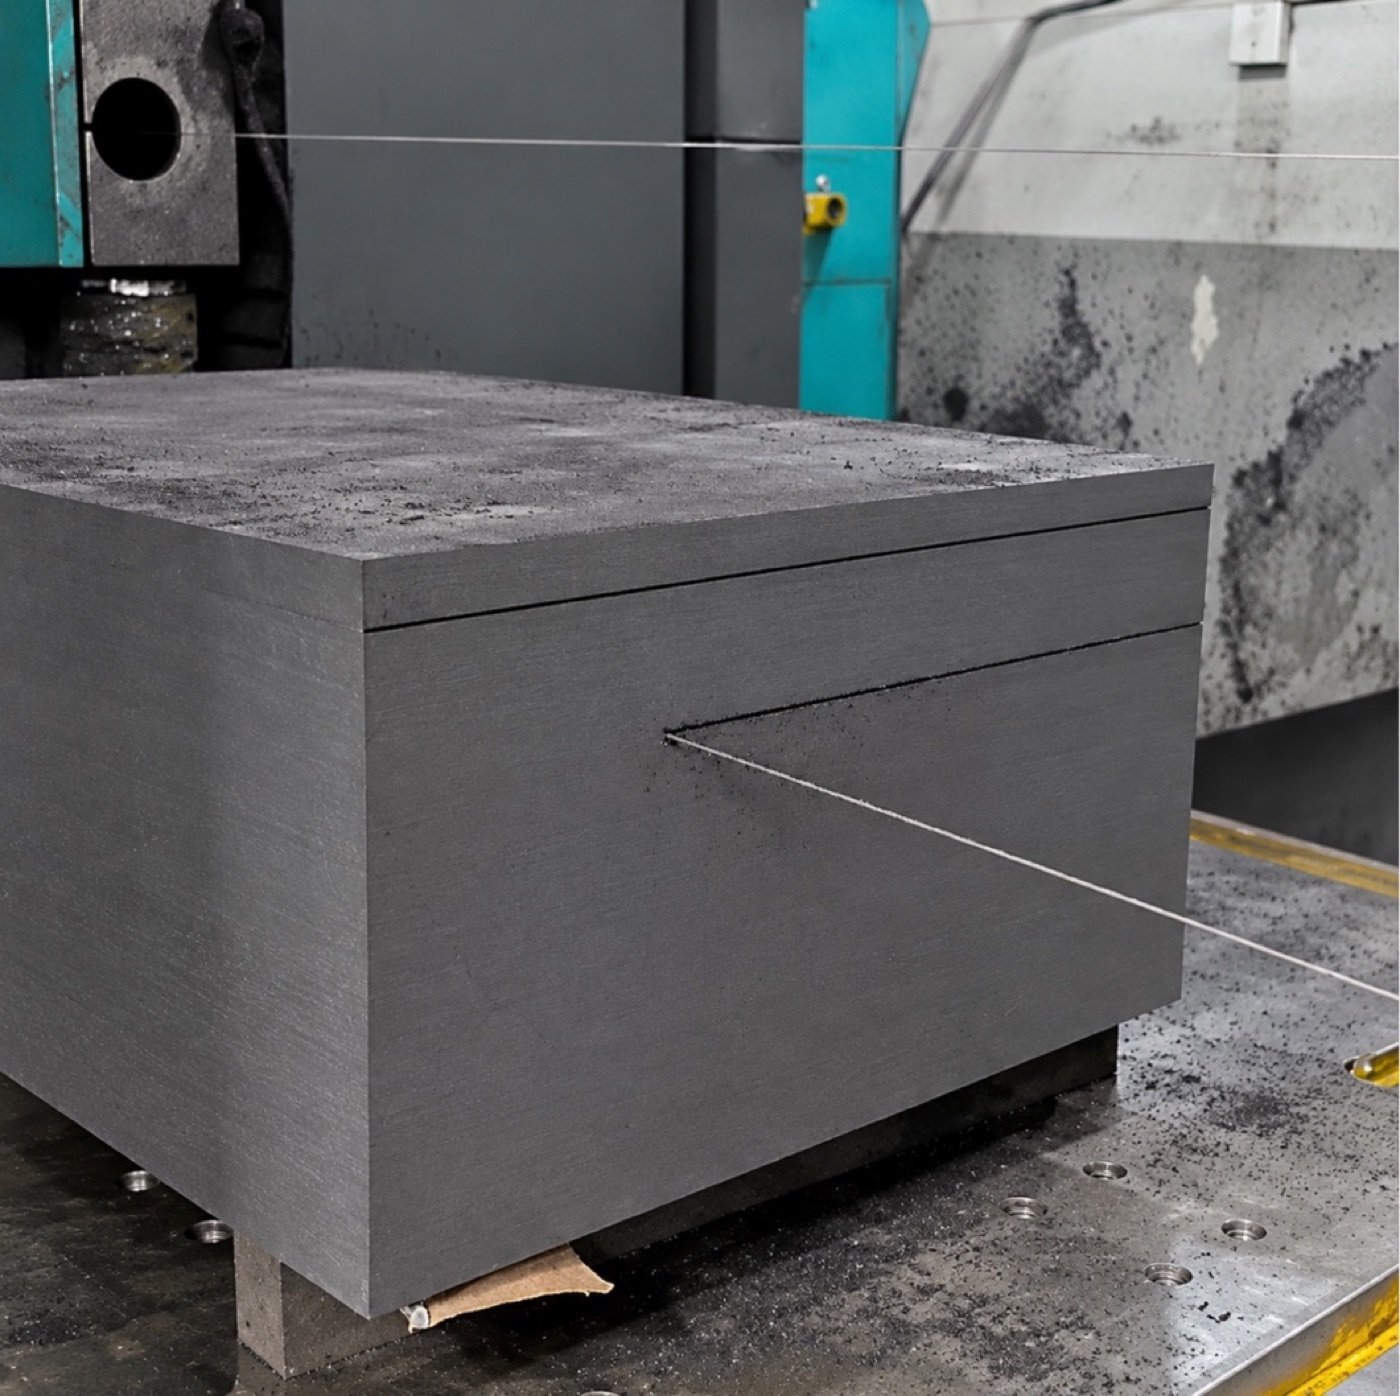
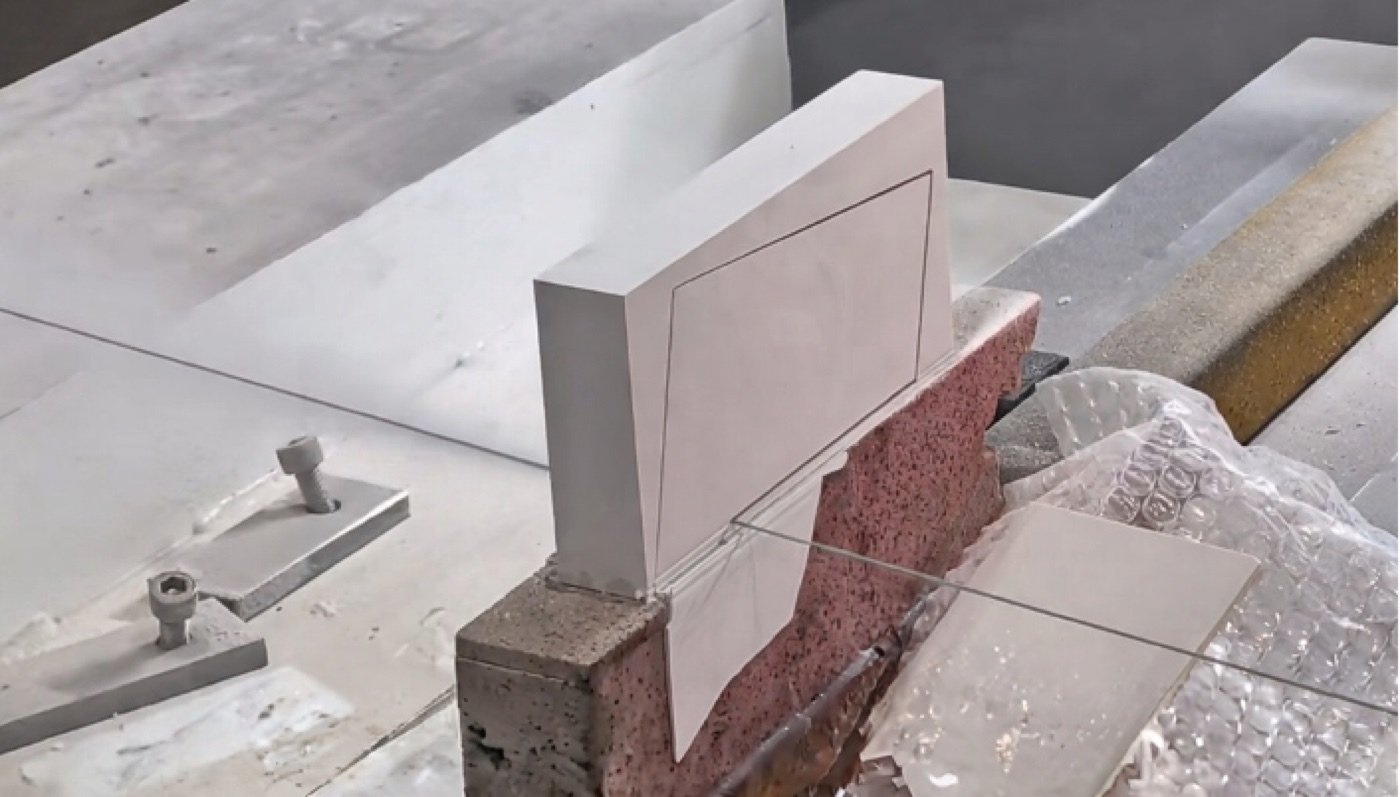
切断サンプルと受け入れ検査

作業面にクランプされた切断サンプル
機器ドキュメントからの追加サンプルビュー

試験切断中に確認すること

送り速度または切断方向を選択する前に、完成したブランクの寸法と機械加工代について合意してください。合意した位置での基準面、エッジの状態、および寸法変動を検査してください。結果の再現性を確保するために、グラファイトグレード、切断方向、およびサポートを記録してください。

グラファイト切断セットアップ

一般的な材料には、等方性、押出成形、および微粒グラファイトが含まれます。SHGシリーズはグラファイトを乾式で切断します。切断ゾーンでの集塵を計画し、ブロック寸法に対するワークピースサポートと固定を確認してください。

等方性および微粒グラファイトの場合、初期プロセスウィンドウはワイヤ速度30〜40 m/s、送り速度50〜100 mm/minです。初期ワイヤ径と張力範囲は0.6〜1.0 mmおよび150〜200 Nです。機械のワイヤ速度範囲は0〜50 m/sです。実際のグレードと断面サイズに合わせて、コミッショニング中に生産パラメータを設定してください。

よくある質問

3 mのグラファイトブロックに適したモデルはどれですか?

SHG330-120は、単一切断モードで最大3,300 mm長のブロックに対応し、公称エンベロープは3,300 × 1,200 × 1,000 mmです。複合モードの長さ制限は2,500 mmです。

同じブロックを水平および垂直に切断できますか?

はい。個別の切断ユニットが1つのフレームに取り付けられています。切断計画を確定する前に、選択したモデルの複合モードエンベロープを確認してください。

機械はプロファイル加工されたグラファイトブランクを切断できますか?

同期X/Z補間は、プログラムされた輪郭切断をサポートします。実現可能性を確認するために、プロファイル図を共有してください。

グラファイト切断にはクーラントが必要ですか?

SHGグラファイトプロセスは乾式です。切断ゾーンに集塵を提供してください。

Vimfunは異なるブロックサイズの機械を製造できますか?

X、Y、Zトラベル、ワークテーブルの寸法、固定、および集塵インターフェースは、設置に合わせて仕様を決定できます。

SHG構成と見積もりをリクエストする

ワークピースと出力

  • グラファイトグレードと最大ブロックサイズ(長さ×幅×高さ)
  • ブロック重量と積載方法
  • 切断方向、部品図、およびシフトあたりの出力

設置

  • 電源と設置面積
  • 集塵および排気接続

SHG構成について相談する

SHG見積もりをリクエストする
トップに戻る