Slab and plate cutting
Feed the cutting head down through the block to separate slabs or part off sections.

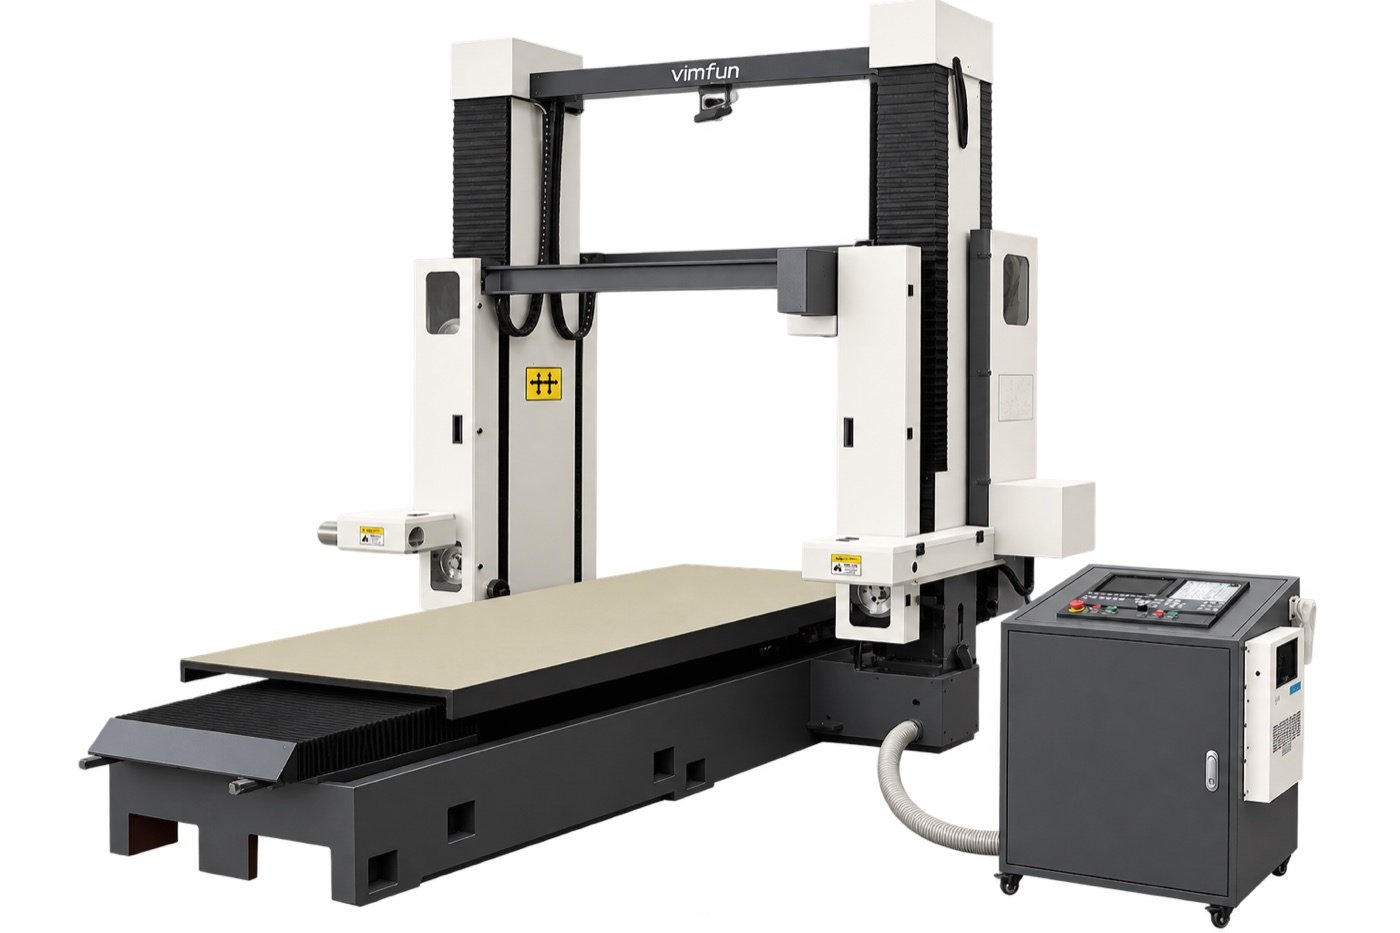
The SHG series cuts large graphite blocks into slabs, plates and profiled blanks. Separate horizontal and vertical cutting heads travel above a low, stationary table, so the block can stay in the same setup when switching cutting directions.
Choose from four standard models by the required cutting mode and full block dimensions. Standard capacity reaches 3,300 mm in a single mode and 2,500 mm in combined mode.
Use the SHG as a graphite block slabbing machine for straight cuts. Compare the working envelopes for horizontal and vertical graphite cutting before choosing a model.
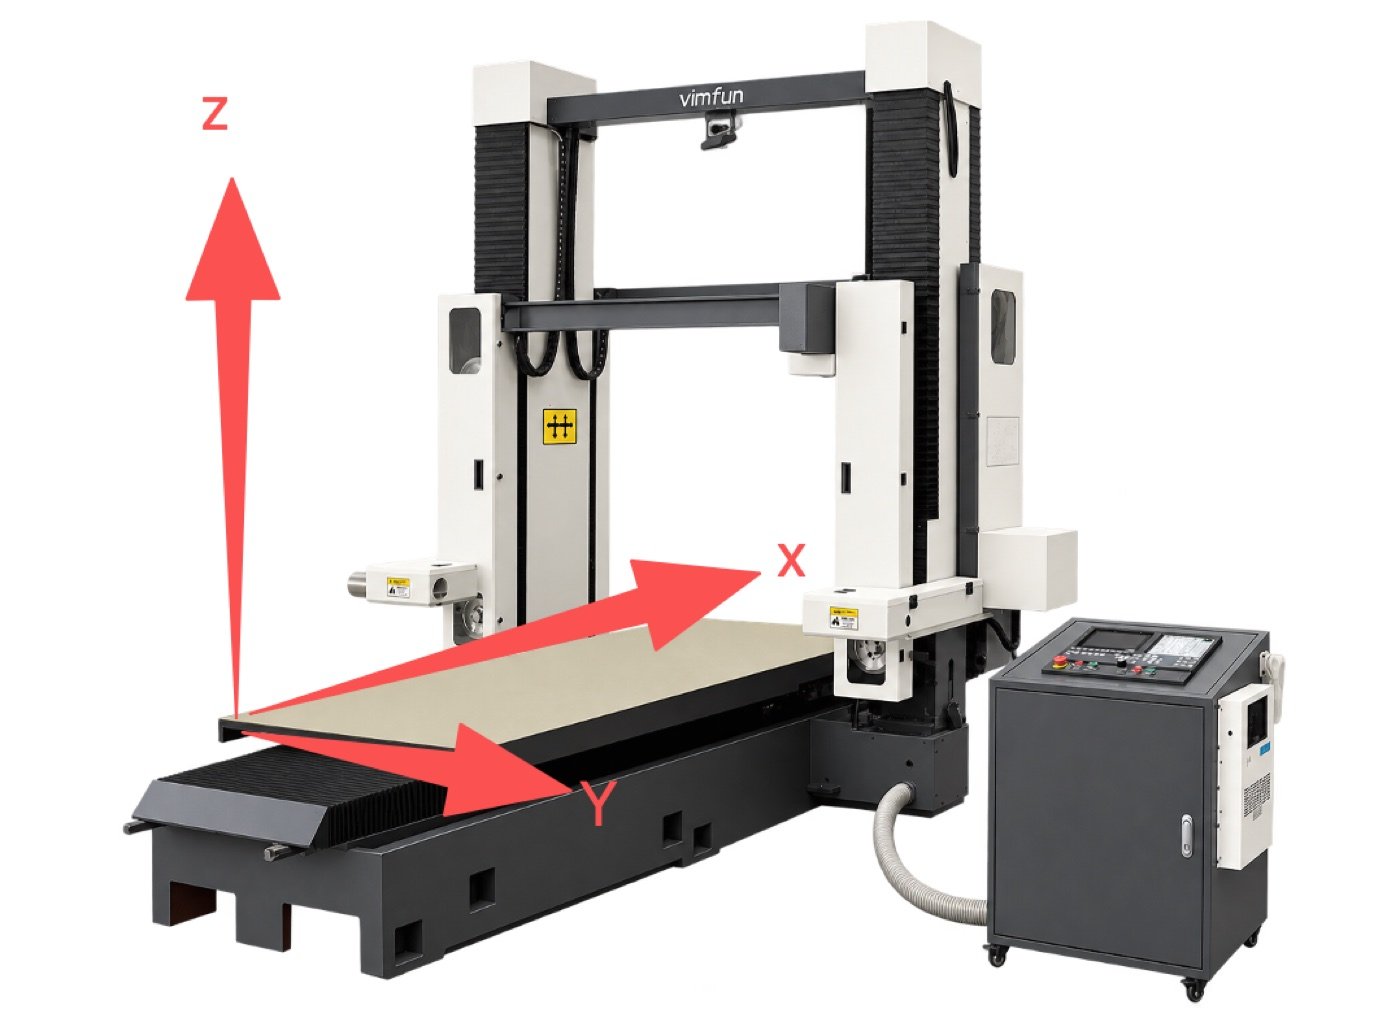
The SHG holds the graphite block stationary on a low table. Two independent cutting assemblies move on the gantry, each with its own closed-loop cutting wire. The numbers in the schematic match the component list below.
| Axis | Arrow in schematic | What moves | 機能 |
|---|---|---|---|
| X | Front to back, along the block length | Cutting assemblies travel front to back along the block length; both units share this longitudinal travel. | Squaring, trimming and long straight cuts. |
| Y | Left to right, across the block width (along the beam) | Cutting assemblies move across the width of the workpiece. | Positioning the cut across the width of the block. |
| Z | 縦型 | Vertical travel of the cutting assembly. | Top-down feed for slabbing and separating sections. |
| X + Z | Coordinated motion | Both axes move at the same time under CNC control. | Programmed contour cuts for shaped blanks. |
Share the profile drawing so Vimfun can confirm feasibility and fixture clearance.
m/s. How fast the closed-loop wire circulates around its loop. It is set by the wire drive.
Machine range: 0–50 m/s. Initial window for isostatic and fine-grain graphite: 30–40 m/s.
mm/min. How fast CNC motion advances the cutting assembly relative to the block, which is how fast the cut progresses through the graphite.
Machine range: X 0.01–3000 mm/min; Y and Z 0.01–5000 mm/min. Initial window for isostatic and fine-grain graphite: 50–100 mm/min.
Wire speed is the motion of the cutting tool itself. Feed rate is the motion of the axes. At the initial window, the wire travels roughly 18,000 to 48,000 times farther per minute than the head advances. Raising wire speed does not advance the cut, and raising feed does not make the wire run faster. Set both during commissioning for the actual grade and section size.
Single-mode length matches the X travel of the model. When the horizontal and vertical units work in the same setup, both assemblies share the same X stroke instead of each having the full stroke. The block must therefore fit a shorter envelope. On the standard models, the combined-mode length is 600 to 800 mm below the single-mode length.
A 2,400 × 1,400 × 1,200 mm block requiring both directions puts the SHG300-170 on the shortlist. Its combined-mode length and width match the nominal block size. Confirm usable height, actual stock dimensions and support clearance before selecting it. The SHG330-120 has a 1,200 mm combined-mode width, so this block exceeds its width limit.
Locate the block from a stable datum, check support under the cut-off section, and allow space for dust extraction and handling before the first pass.
これらの画像は、SHG機器の推奨事項からのものです。意図された操作を確認する際には、容量表と併せて使用してください。
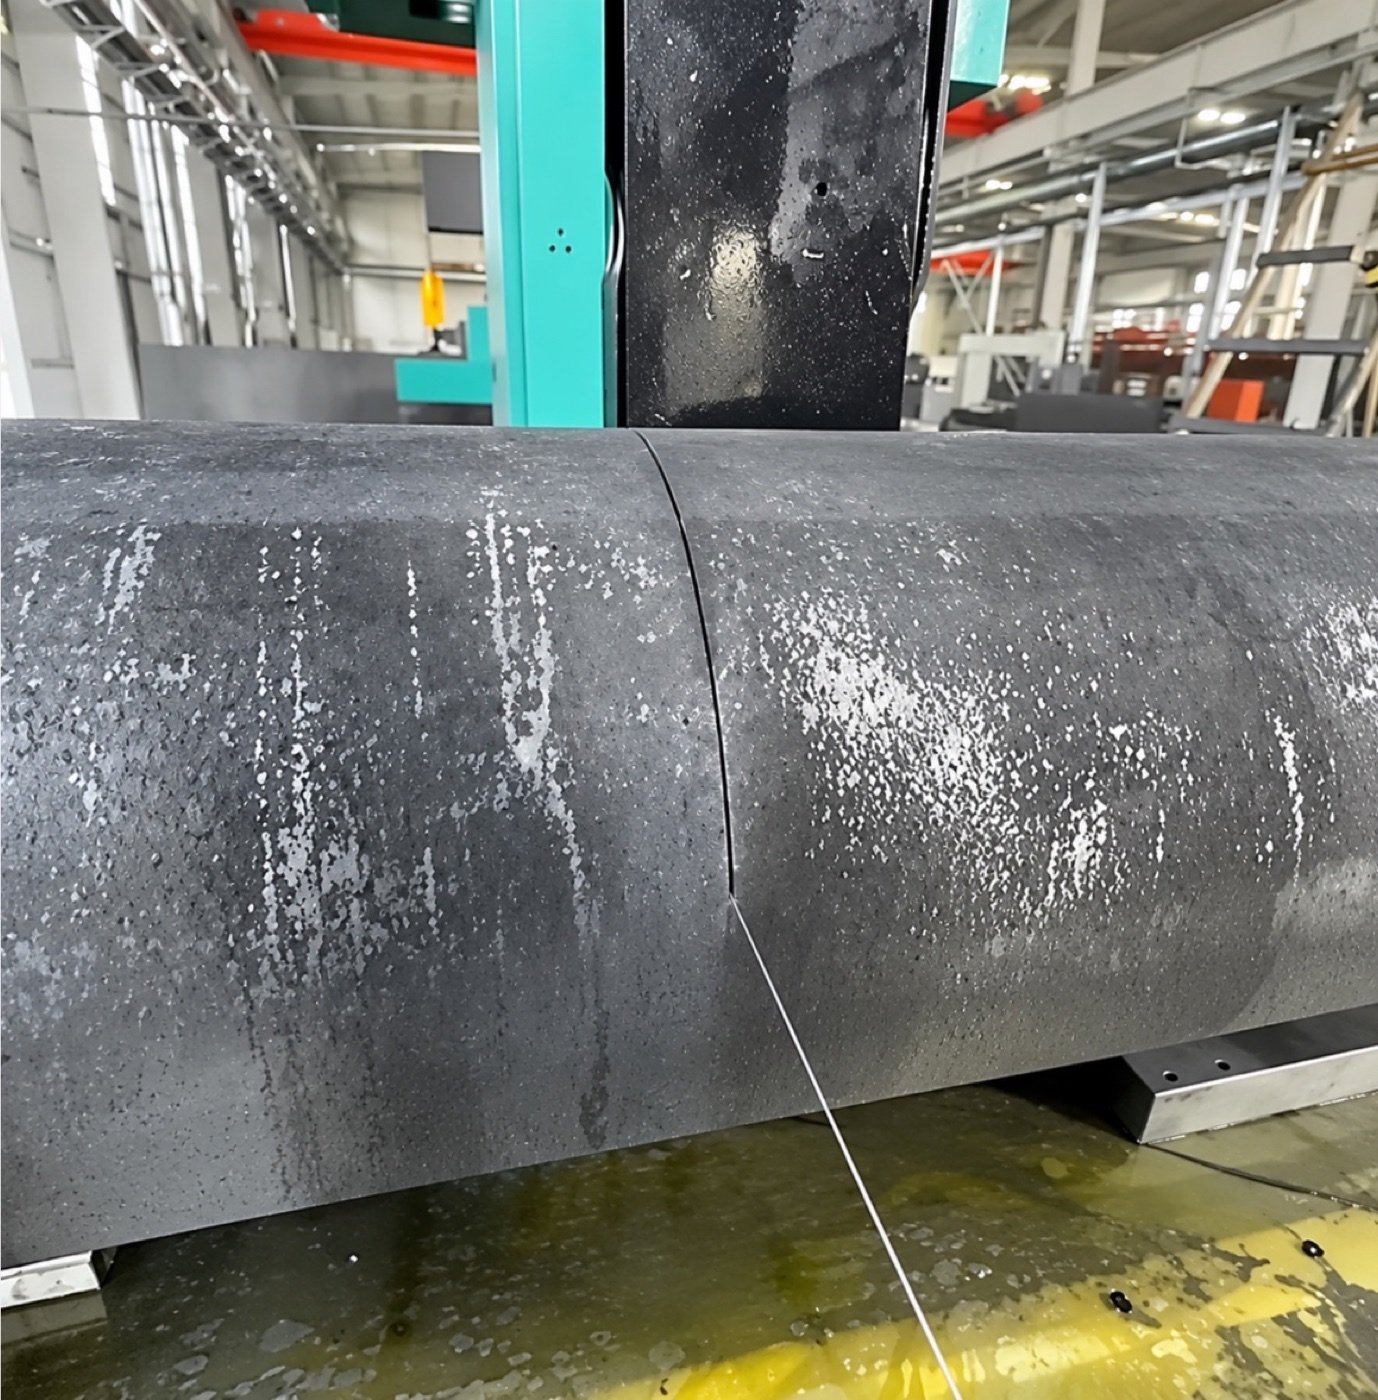
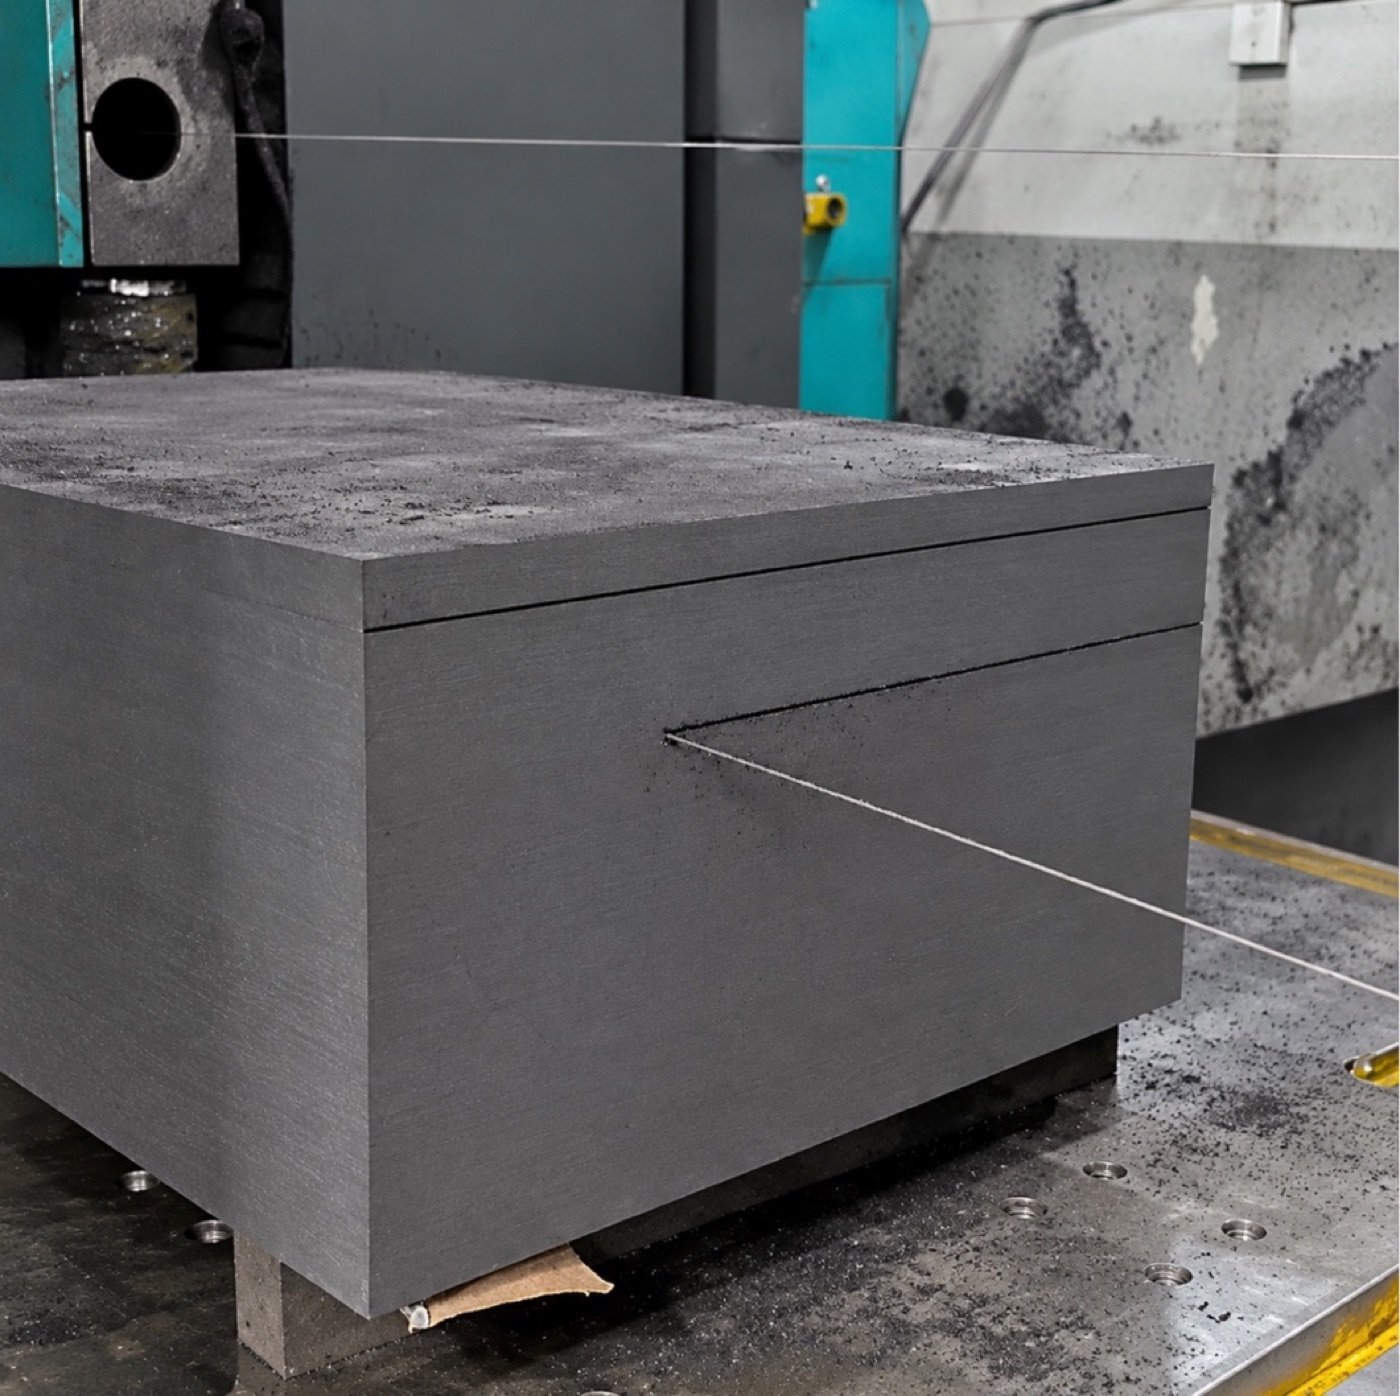
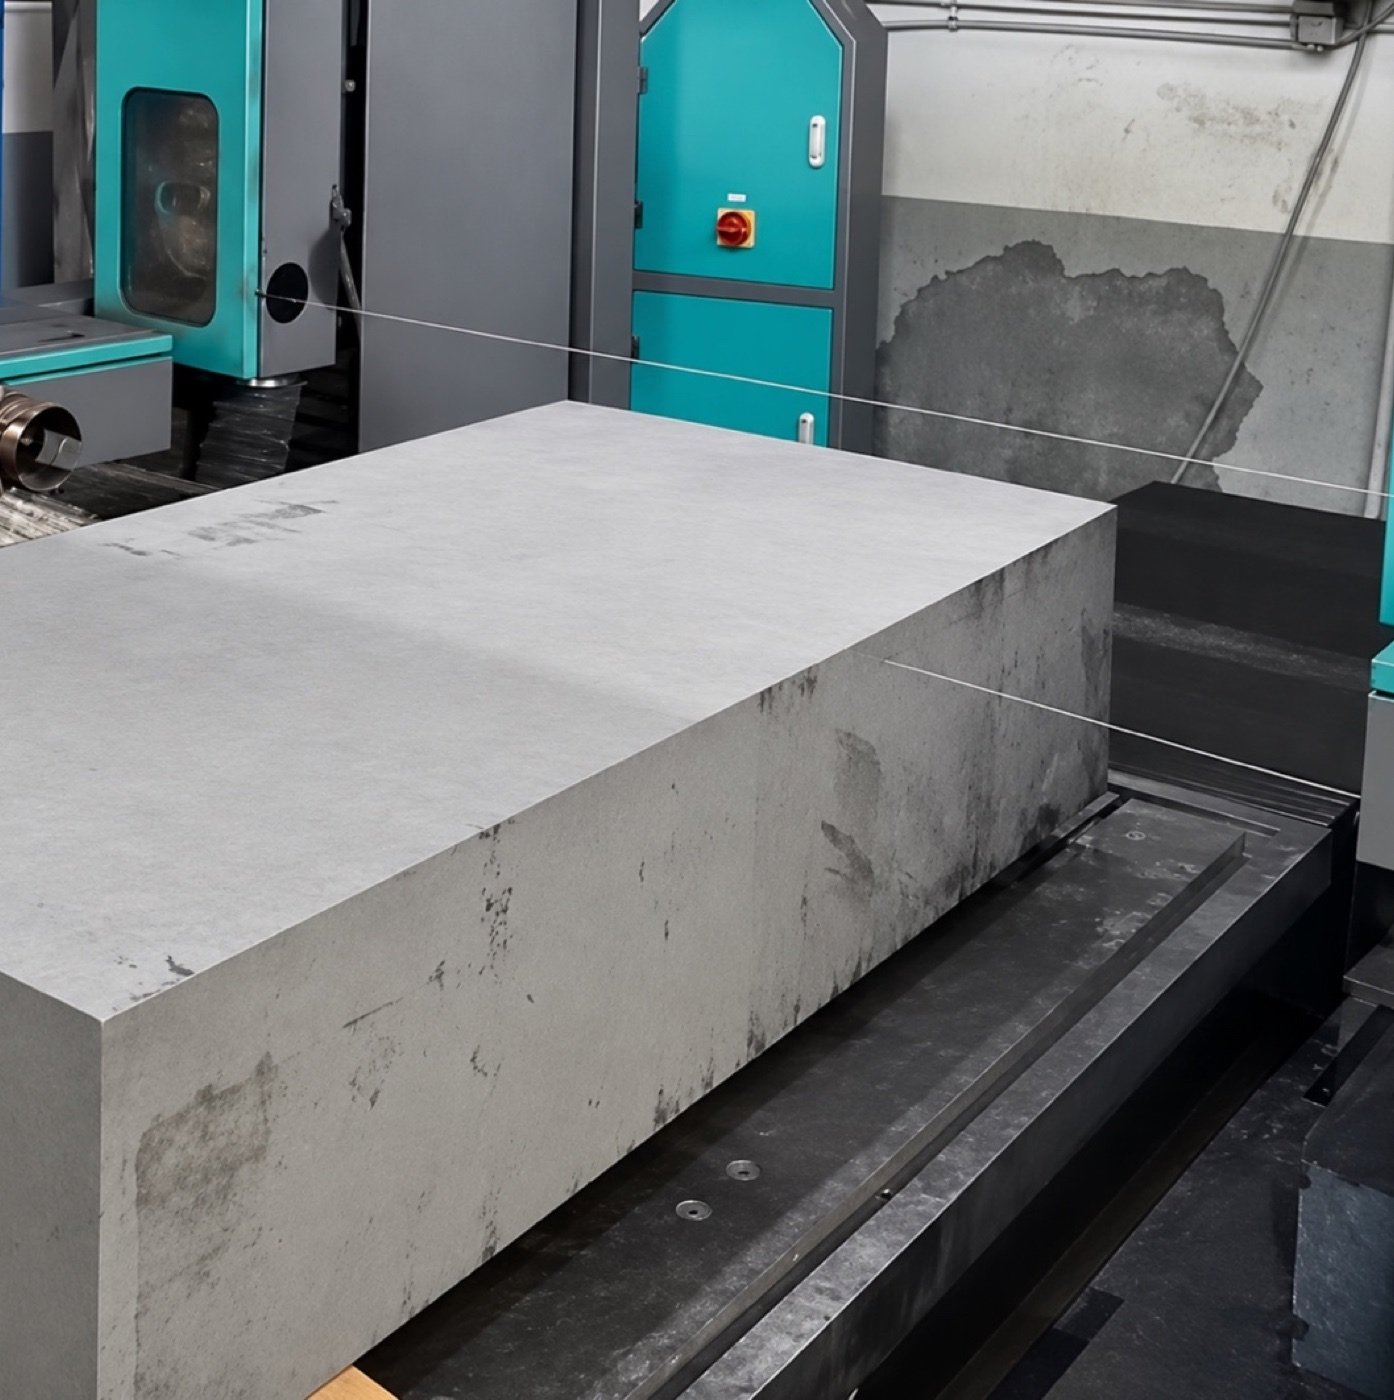
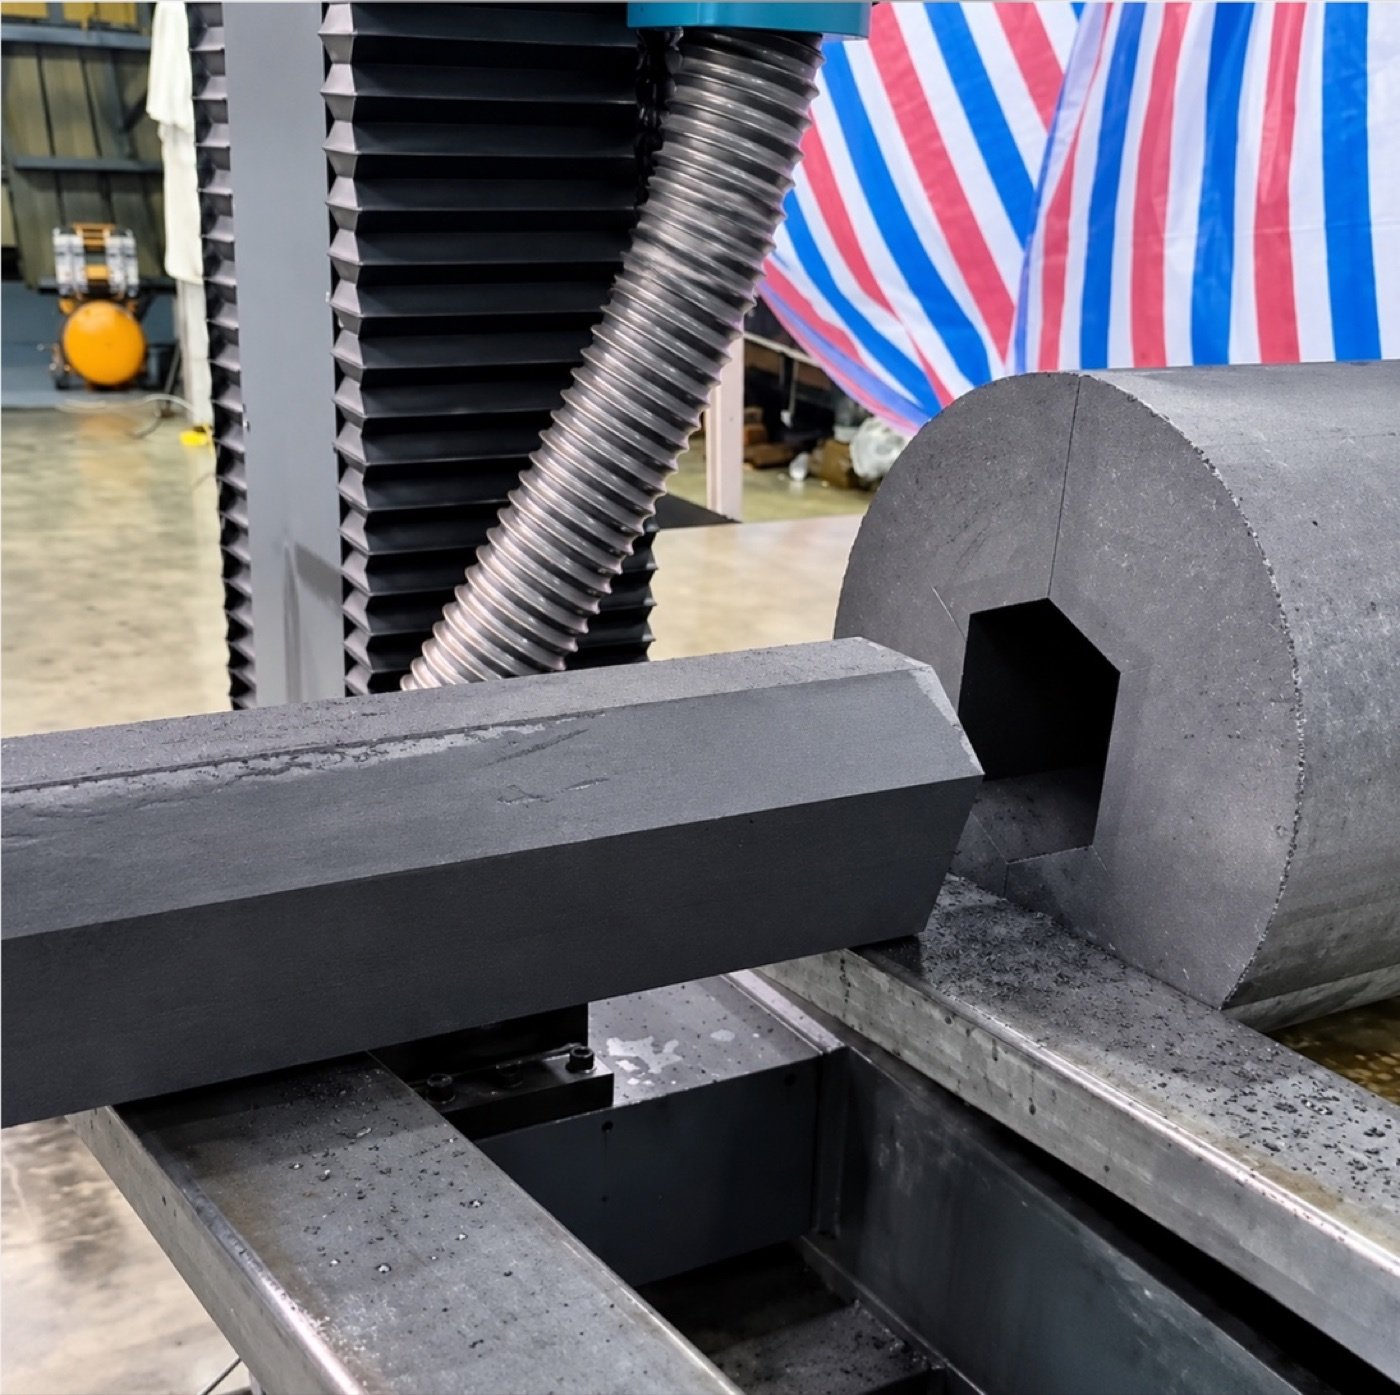
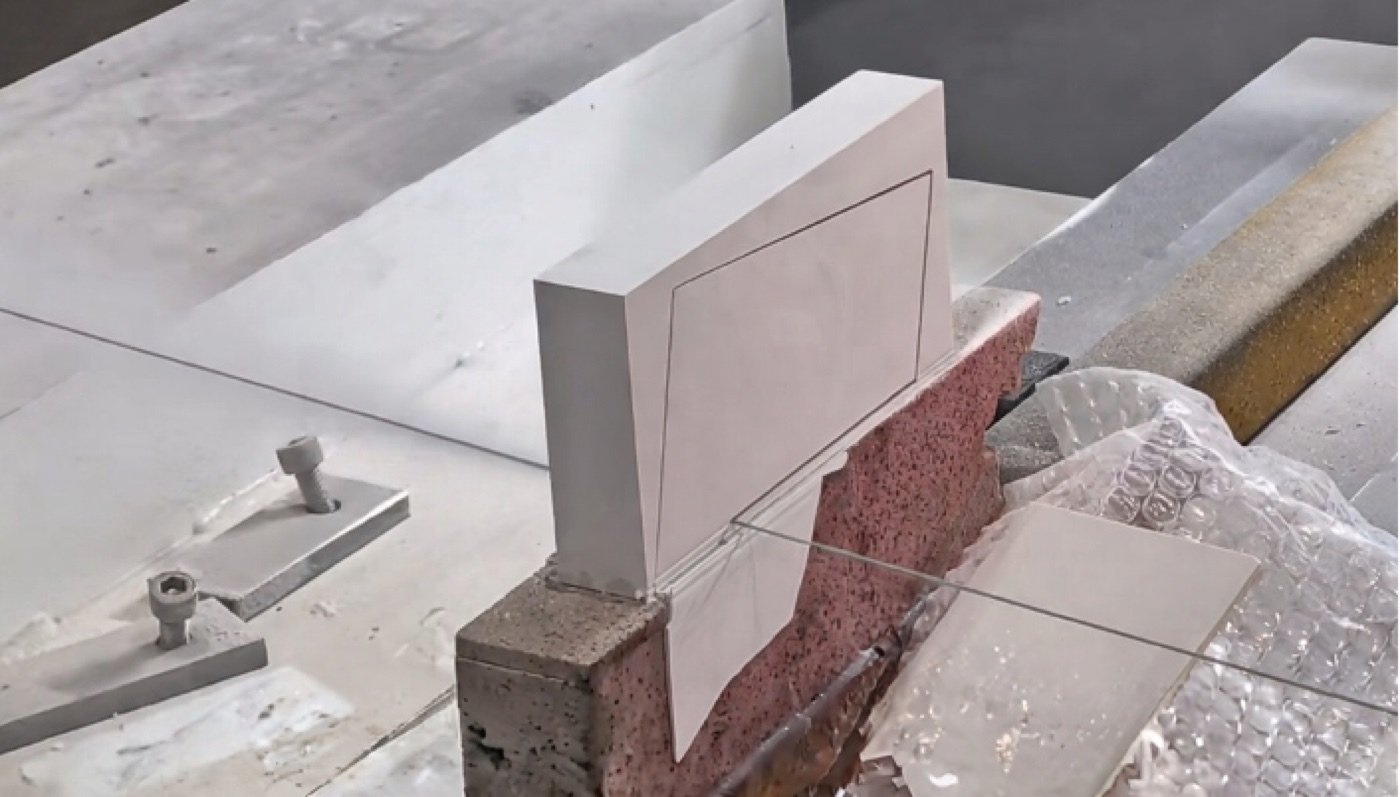
送り速度または切断方向を選択する前に、完成したブランクの寸法と機械加工代について合意してください。合意した位置での基準面、エッジの状態、および寸法変動を検査してください。結果の再現性を確保するために、グラファイトグレード、切断方向、およびサポートを記録してください。