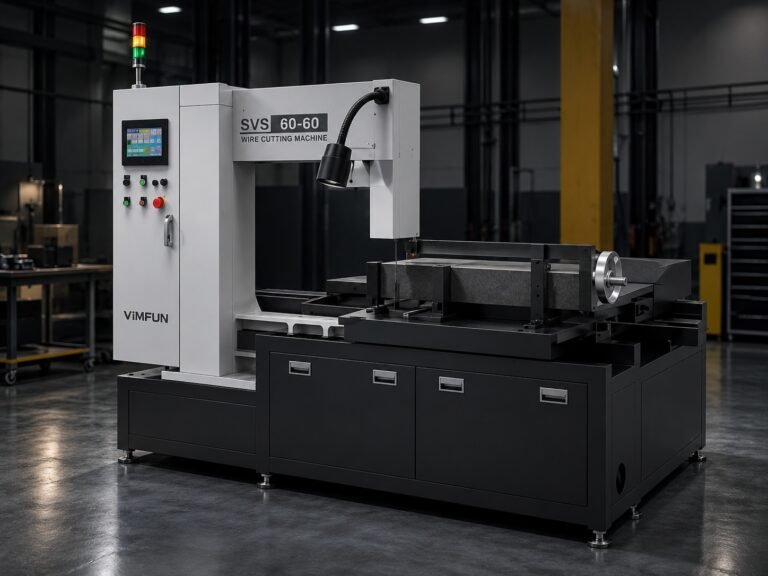
If you’ve been told a wire saw can hold ±0.01 mm on graphite, ask for the data. In our experience running SV60-60 and SH60-60 machines on isostatic and fine-grain graphite, the sustained production tolerance with wire-saw cutting sits at ±0.03 mm — reliably, across a full shift, without babysitting every cut. That is a real number backed by process validation, not a spec sheet aspiration.
The question isn’t just “how accurate can you get?” It’s “how accurate do you need, and what does achieving that cost you in throughput, wire consumption, and process complexity?” Those two questions have different answers depending on whether you’re cutting semiconductor graphite boats, EDM electrodes, or industrial furnace components. This article walks through each accuracy dimension, the parameters that control it, and the honest trade-offs at each precision tier.
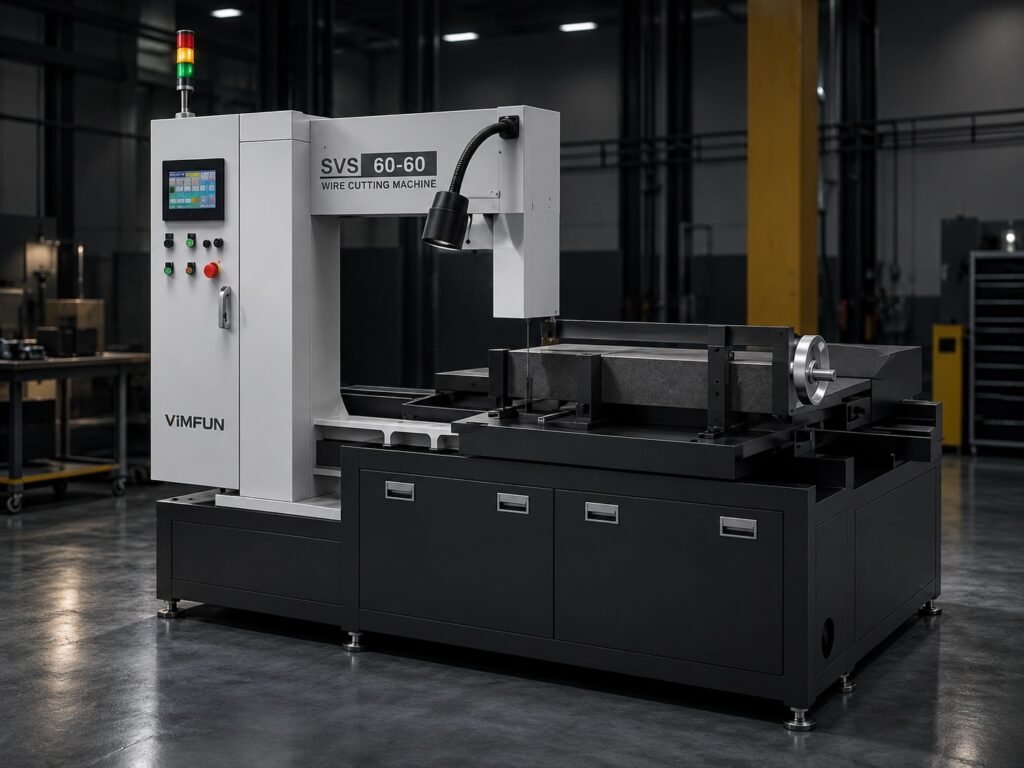
VIMFUN’s SV60-60 and SH60-60 wire saws are the machines this article is built around. Both are purpose-configured for graphite: vertical or horizontal orientation, 0.6–1.0 mm diamond wire, dry cutting (no coolant), and a wire tension range of 150–200 N that keeps dimensional scatter under control batch after batch.
1. Defining Accuracy in Graphite Cutting
Accuracy in graphite cutting is not one number. Buyers and process engineers use the word loosely, and that ambiguity causes misaligned expectations on both sides of a purchase decision. Before specifying a tolerance requirement, it helps to agree on which kind of accuracy you actually mean.
There are three distinct dimensions:
Dimensional accuracy — the absolute size tolerance on length, width, or thickness. This is what most people mean when they say “±X mm.” It tells you how close the actual cut dimension is to the nominal.
Form accuracy (geometric accuracy) — flatness, parallelism, squareness. A part can be dimensionally within spec but still be out of tolerance on flatness if the cut surface is bowed or if two opposing faces aren’t parallel to each other.
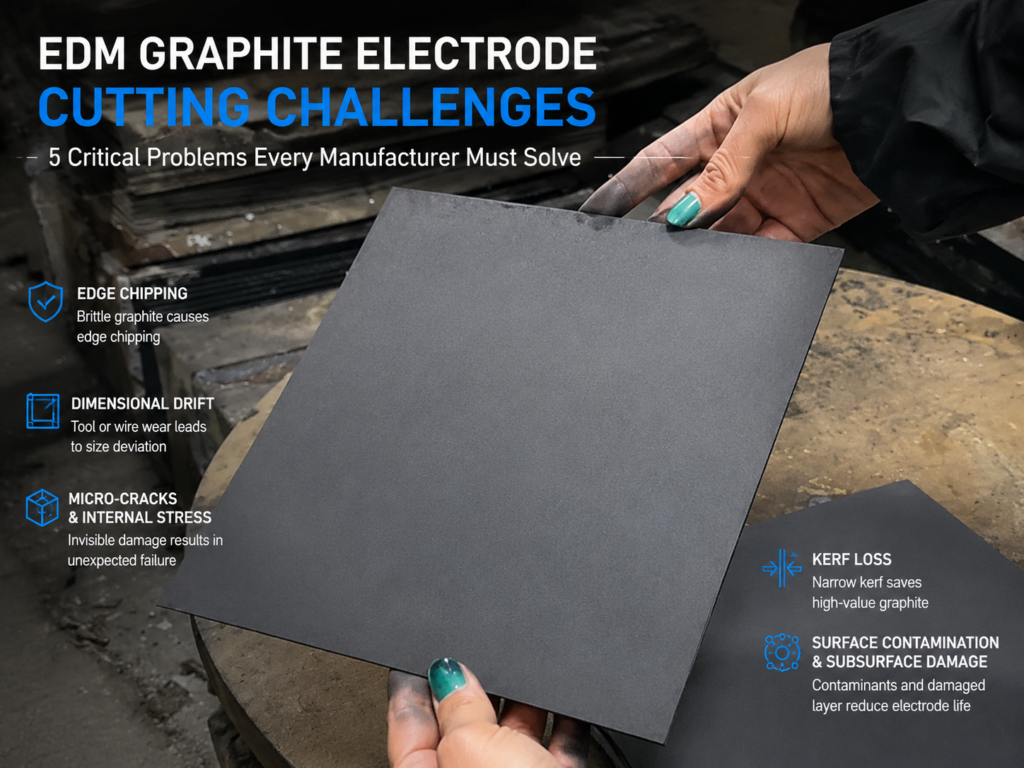
Surface accuracy — surface roughness (Ra) and edge integrity. Graphite is brittle; edge chipping and micro-cracking are real failure modes that dimensional tolerance specs don’t capture.
Wire sawing addresses all three, which is one of the reasons it has displaced band saws and ID saws in demanding graphite applications. For a broader view of how wire cutting compares to other methods, see our guide to precision graphite slicing and the comparison of graphite machining alternatives.
Three Practical Accuracy Tiers
Based on application requirements across our installed base, graphite cutting divides into three tiers:
| Tier | Tolerance | Typical Application |
|---|---|---|
| Semiconductor-grade | ±0.01 mm | Graphite boats, susceptor rings for epitaxial deposition |
| EDM-grade | ±0.05 mm | EDM electrodes, precision mold components |
| Industrial-grade | ±0.1 mm | Furnace parts, structural graphite, thermal management blocks |
Wire sawing with the VIMFUN SV60-60 achieves ±0.03 mm in sustained production — which sits between semiconductor-grade and EDM-grade on this table. Reaching ±0.01 mm requires a downstream finish step (typically precision grinding). Attempting it on the wire saw alone without downstream processing is where teams run into inconsistency.
2. What Controls Accuracy in High Accuracy Graphite Cutting
Four factors drive dimensional outcome on a wire saw. Miss any one of them and your tolerance spec becomes a theoretical exercise.
Mechanical System Baseline
The machine’s own positional accuracy sets the floor. Feed axes need sub-micron repeatability; any play in the guide system or wire anchor shows up directly as dimensional scatter. The VIMFUN SV60-60 is built for ±0.03 mm as a sustained production tolerance — meaning the mechanical baseline is tighter than the published spec by enough margin to absorb normal process variation.
One thing that’s easy to underestimate: thermal expansion in the cutting frame. During a long production run, frame temperature can drift by a few degrees. At those scales, thermal expansion of the workpiece fixture itself becomes a non-trivial contributor to dimensional error. This is one reason we recommend letting the machine reach thermal equilibrium before starting a tight-tolerance batch — it’s a 20-minute wait that saves a lot of rework.
Wire Speed: 40–70 m/s
Wire speed affects both material removal rate and surface quality. At the lower end of the range (40–45 m/s), you get more aggressive cutting but a rougher surface and more edge chipping on fine-grain graphite. At the upper end (65–70 m/s), surface quality improves noticeably and edge sharpness is better, but you’re also asking more of the wire over its service life.
For high accuracy graphite cutting, we generally start around 55–60 m/s for isostatic graphite and adjust from there based on material grade. Jumping straight to 70 m/s on a new material without qualification is the kind of shortcut that generates a bad batch at 3 AM.
Feed Rate: 50–100 mm/min
Feed rate is the most direct accuracy lever available to the operator. Slower feed means more wire contact time per unit thickness, finer surface, and less lateral force on the wire — all of which improve dimensional consistency.
The practical lower limit around 50 mm/min is set by productivity. Below that, you’re not making enough progress to justify the machine time. The upper end at 100 mm/min is where you start to see wire bow become significant enough to affect dimensional output on thin slices. For tight-tolerance work (targeting ±0.03 mm sustained), 60–75 mm/min is the sweet spot on most isostatic graphite grades.
Wire Tension: 150–200 N
This is the parameter that gets the least attention and causes the most problems in my experience. Tension controls wire bow under cutting load. Too low, and the wire deflects laterally — your cut plane angles, your dimensional output degrades, and you can’t figure out why because the symptom looks like a calibration problem. Too high, and you’re accelerating wire fatigue. The wire’s rated life of approximately 7 days at 8 hours/day (roughly 56 operating hours) assumes tension stays in the 150–200 N window.
Dry Cutting Strategy
Graphite is cut dry on the SV60-60 and SH60-60 — no liquid coolant. This is a deliberate process choice, not a limitation. Liquid coolant would contaminate the graphite, cause absorption in porous grades, and create graphite-slurry disposal problems. The trade-off is dust management: dry cutting generates fine graphite particulate that requires a dedicated extraction system.
Teams that try to skip the dust extraction step to save setup time discover quickly that accumulated dust in the machine affects wire tracking and can accelerate guide wear. That’s a fixable problem, but it’s not free.
3. Multi-Dimensional Accuracy: Size, Form, and Surface
High accuracy graphite cutting means controlling all three dimensions simultaneously — not just hitting a dimensional number.
Dimensional Accuracy (Size)
On length, width, and thickness, the VIMFUN SV60-60 holds ±0.03 mm in sustained production on isostatic and fine-grain graphite. This applies to cuts from thin wafer slices through thick block sections. The key requirement is that workpiece fixturing is rigid — graphite is light, but vibration from an undersized fixture shows up in dimensional scatter.
Form Accuracy (Flatness and Parallelism)
Wire saws produce flat, parallel cut faces as a natural consequence of the process geometry. The wire moves in a single plane; if the workpiece feed is perpendicular to that plane, the resulting cut faces are parallel to each other and perpendicular to the feed direction.
For low-kerf graphite cutting applications where thin slices are being cut from valuable blocks, this inherent flatness is particularly important: a bowed slice cannot be corrected without additional machining, which defeats the purpose of minimizing kerf loss in the first place.
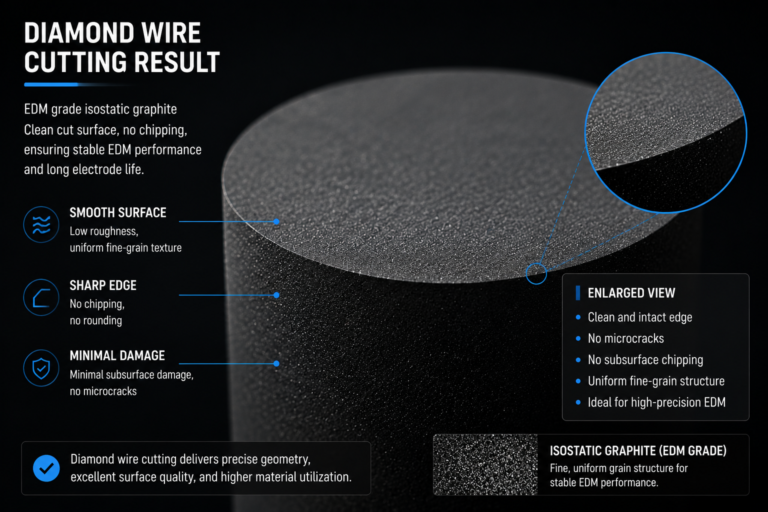
Practical flatness and parallelism on wire-sawn graphite: flat, uniform faces with no edge chipping — consistent across the cut surface without post-processing.
Surface Quality (Ra and Edge Integrity)
Surface roughness on wire-sawn graphite depends on wire diameter, speed, and feed rate. With 0.6–0.8 mm wire at 55–65 m/s and moderate feed, the resulting surface is smooth and uniform, without the edge microcracks that ID saws and abrasive band saws tend to leave on brittle graphite grades.
Edge chipping — the failure mode where corners and edges break away during or after cutting — is essentially eliminated at the recommended parameters. This matters most for semiconductor graphite boats, where edge integrity affects how the boat handles wafer loading without generating particles.
Wire diameter selection has a direct effect on surface quality and is worth discussing explicitly. A 0.6 mm wire produces a narrower kerf (less material loss) and a finer surface finish, but it is more sensitive to tension and feed rate variation — the tolerance window for correct process setup is narrower. A 1.0 mm wire is more forgiving, tolerates slightly faster feed, and is better suited to larger workpieces where stiffness helps maintain wire tracking. For high accuracy graphite cutting where surface quality is the priority, 0.6–0.8 mm is the typical selection range. For applications where throughput matters more than ultimate surface quality, 0.8–1.0 mm makes more sense.
One limitation worth naming: surface roughness from wire sawing alone is typically not at the level required for polished optical or precision contact surfaces. If a very low Ra value is required after cutting, a lapping or grinding step will still be needed. Wire sawing gets you close; it does not replace surface finishing for the highest-spec graphite components. This is an honest constraint, and any process that claims otherwise should be asked for Ra data across a production batch.
4. Maintaining Accuracy in High Accuracy Graphite Cutting Across Long Runs
One-off accuracy is relatively straightforward. Sustained accuracy across a production batch of 50 or 500 pieces is the harder problem, and it’s where equipment quality and process discipline separate the workable approaches from the ones that fail in production.
Wire Diameter Wear and Compensation
Diamond wire wears over its service life. As the wire diameter decreases, kerf width decreases — which sounds like it would improve material yield, but actually introduces a dimensional drift if the wire compensation isn’t tracked. A wire that started at 0.8 mm and has worn to 0.72 mm will produce parts that are systematically different from the specification if no compensation is applied.
The VIMFUN SV60-60 tracks wire wear and allows offset compensation. The wire’s service life is approximately 7 days at 8 hours/day — after which replacement is required regardless of apparent condition, because fatigue accumulation in the wire core isn’t visible. Teams that try to extend wire life beyond this window to save consumable cost typically discover the problem in a batch of out-of-spec parts, not before.
Batch-to-Batch Consistency
The factors that affect batch consistency are: wire condition (age, accumulated wear), fixture condition (clamping force, thermal state), and room temperature if ambient swings are large. In a controlled production environment, these are manageable. In an uncontrolled one, dimensional scatter of ±0.05 mm or worse becomes common even on a machine capable of ±0.03 mm.
Repeatability — the ability to return to the same dimensional output on a new batch with fresh wire — is where machine quality shows. On the SV60-60, positional repeatability is tight enough that batch-to-batch dimensional variation is dominated by process inputs (wire condition, fixturing), not machine variation.
Fixture Design Is Underrated
The workpiece fixture doesn’t move — but its design directly affects the cut. Graphite is soft enough that clamping pressure can cause micro-distortion in the workpiece, particularly in thin sections. If the part is distorted in the fixture during cutting and then springs back when unclamped, what measured as in-tolerance on the machine can come out of tolerance in inspection. This is one of those issues that bites teams who adapt fixtures from harder materials without rechecking clamp force limits.
For repeated production runs of the same graphite component, investing in a custom fixture that correctly distributes clamping load pays back quickly. It’s the kind of detail that doesn’t appear in machine specifications but has a measurable effect on sustained dimensional output. The applications engineering team at VIMFUN typically reviews customer fixture designs before first production runs — and this is not a formality.
5. Application Requirements: Where High Accuracy Graphite Cutting Matters Most
Different applications demand different things from a cutting process. A tolerance requirement that is critical for one application is irrelevant for another — and understanding this drives better equipment selection decisions.
Where Each Application Sits vs. Related Pages
| Application | Tolerance Need | Key Constraint | Related Page |
|---|---|---|---|
| Semiconductor graphite boats | ±0.01–0.03 mm | Edge integrity, particle generation | graphite boat cutting |
| EDM electrodes | ±0.05 mm | Geometry accuracy, surface finish for EDM spark gap | EDM graphite electrode cutting |
| Industrial furnace parts | ±0.1 mm | Throughput, cost, material utilization | general cutting pages |
| Thin slices / wafers | ±0.03 mm + flatness | Kerf loss, flatness | low-kerf graphite cutting |
Semiconductor Graphite Boats — Highest Precision
Graphite boat cutting for semiconductor applications sits at the top of the accuracy pyramid. Boats used in CVD, epitaxial growth, and diffusion furnaces must hold tight slot dimensions to accept wafers without lateral play, while also maintaining edge integrity to prevent particle generation inside the process chamber.
Wire-saw cutting with the SV60-60 produces the flat, chip-free surfaces these parts require. Dimensional tolerance at ±0.03 mm on the wire saw, followed by precision grinding where ±0.01 mm is required, is the two-step process most qualified manufacturers use.
EDM Electrodes — Geometry and Surface Matter
EDM graphite electrode cutting operates at ±0.05 mm tolerance in most cases. The geometry of the electrode directly determines the shape burned into the workpiece — a twisted or bowed electrode face creates a distorted cavity. Wire sawing is well-suited here because the resulting faces are flat and the cut angles are controlled.
Surface roughness also matters for EDM: a smoother electrode surface produces a more predictable spark gap. Wire-sawn graphite surfaces are suitable for most EDM applications without additional finish grinding.
Industrial Graphite Components
At the industrial end — furnace parts, heat shields, structural blocks — the tolerance requirement relaxes to ±0.1 mm or wider. Here the economic driver shifts: throughput and material utilization matter more than dimensional perfection. Wire sawing is still used for low-kerf graphite cutting to maximize material yield from expensive graphite stock, but the accuracy bar is more forgiving.
6. The Economics of Accuracy: When Tighter Isn’t Better
There is a cost curve attached to every tolerance tier. The relationship is not linear: going from ±0.1 mm to ±0.05 mm costs a moderate increment. Going from ±0.05 mm to ±0.01 mm costs a large increment. Going below ±0.01 mm costs an enormous increment that most applications cannot justify.
The Cost Components of Tight Tolerance
Throughput. Slower feed rates for tighter tolerances reduce parts-per-hour. At 60 mm/min vs. 100 mm/min, you’re accepting 40% lower throughput on the same machine.
Wire consumption. Tighter tolerance work often requires more conservative wire replacement intervals to avoid dimensional drift from wear. Wire is a significant consumable cost.
Process engineering time. Getting to ±0.03 mm consistently requires process qualification: parameter development, fixture design, thermal management. That work is real and front-loaded.
Downstream operations. Reaching ±0.01 mm typically requires wire sawing followed by precision grinding. Two-operation cost vs. one-operation cost.
When ±0.03 mm Is the Right Answer
For most EDM electrode applications and a significant portion of semiconductor graphite boat roughing, ±0.03 mm wire-saw output eliminates the need for a subsequent grinding step. That’s the economic argument for the SV60-60 in these applications: it delivers enough accuracy to be a complete operation rather than a pre-processing step.
If your application genuinely requires ±0.01 mm with no exceptions, plan for a two-step process. If it requires ±0.05 mm, you may be able to run faster and get better throughput than a ±0.03 mm target would allow. Use the tolerance requirement the part actually needs — not the tightest number that sounds impressive in a spec document.
Comparing wire sawing to other methods at various tolerance tiers is covered in more detail at graphite machining alternatives.
7. FAQ
Q: What is the achievable tolerance for high accuracy graphite cutting with a wire saw?
With VIMFUN SV60-60 or SH60-60 machines, sustained production tolerance on isostatic and fine-grain graphite is ±0.03 mm. This applies to dimensional accuracy (length, width, thickness). Reaching ±0.01 mm requires a downstream precision grinding step after wire cutting.
Q: Does high accuracy graphite cutting require coolant?
No. The SV60-60 and SH60-60 cut graphite dry — no liquid coolant. Graphite absorbs liquid and dry cutting avoids contamination. The requirement is a dedicated dust extraction system to handle fine graphite particulate.
Q: How does wire tension affect cutting accuracy in high accuracy graphite cutting?
Wire tension directly controls wire bow under cutting load. At the correct range (150–200 N on the SV60-60/SH60-60), lateral deflection is minimal and dimensional output is consistent. Too low tension causes wire bow that appears as a dimensional or form error — often mistaken for a calibration problem.
Q: How long does diamond wire last in graphite cutting applications?
Wire service life is approximately 7 days at 8 hours per day on graphite with recommended parameters. Beyond this, fatigue accumulation in the wire core creates a fracture risk, even if the wire appears undamaged. Wire replacement at the scheduled interval is part of maintaining consistent high accuracy graphite cutting results.
Q: Is the VIMFUN SV60-60 or SH60-60 better for semiconductor graphite components?
Both machines are configured for graphite and deliver the same ±0.03 mm accuracy. The SV60-60 handles vertical feed orientation, which suits taller workpieces and certain block geometries. The SH60-60 uses a horizontal feed orientation. Selection depends on workpiece shape and fixturing preferences. Contact VIMFUN at daria@endlesswiresaw.com for an application-specific recommendation.
Request a Cutting Accuracy Trial
If you have a graphite component that requires tolerance verification before committing to a production process, VIMFUN offers cutting trials on the SV60-60 and SH60-60. Send your material grade, dimensions, and tolerance requirement to daria@endlesswiresaw.com — the applications team will confirm feasibility and define trial parameters.
About VIMFUN
VIMFUN specializes in endless diamond wire cutting for graphite, advanced ceramics, optical glass, semiconductor materials, and other hard/brittle materials. Machines include the SV60-60 and SH60-60 for graphite applications. Learn more at graphitecutting.com.
About the Author
Written by the VIMFUN Applications Engineering Team — specialists in precision cutting process development for semiconductor, EDM, and industrial graphite applications.