Vimfun・ダイヤモンドワイヤーカット

Industrial Graphite
Block Cutting

Prepare graphite blocks, bars and plates for the next manufacturing step. Plan stock division, support and inspection around the finished geometry and the allowance it needs.

Block divisionBlank preparationInspection & finishing allowance
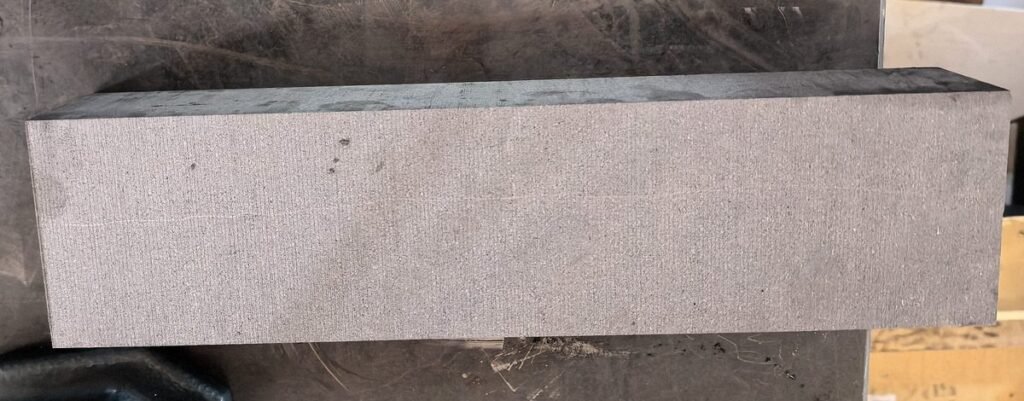
グレード2554の等方性グラファイトバーのダイヤモンドワイヤー切断面
A wire-cut graphite bar from our documented isostatic graphite cutting trial.

From raw stock to a usable blank

Choose the Output Before Choosing the Cut

A rectangular blank, a thin plate and a profiled part need different cutting routes. Block preparation establishes the stock size and reference faces for those later operations.

01

Blocks & bars

Divide stock into rectangular sections for subsequent machining or further cutting. Specify the starting size, required blank size and the faces that will become locating references.

02

Plate stock

Prepare stock for later slicing when thin plates are the final output. Leave enough material for locating and subsequent passes; use a dedicated slicing plan for plate thickness and parallelism.

03

Application blanks

Prepare stock for electrodes, graphite boats or shaped components. Cutting produces a blank; slots, holes, final tolerances and surface requirements may need additional machining.

For thin plate production, continue to our 精密グラファイトスライスガイド. This page focuses on the earlier stock-division stage.

The practical constraints

Control Support, Geometry and Material Loss Together

01

Support through separation

The support arrangement has to remain effective as the cut progresses. Plan how both the remaining stock and the separated piece will be restrained and removed without damaging the cut faces.

02

A repeatable datum

Check the seating faces and their cleanliness before positioning the stock. Reorienting a block between cuts changes the relationship between the locating surface and the next face.

03

A qualified cutting window

Wire condition, tension, feed and the supported cut geometry affect the result. Establish settings through representative cutting and inspection rather than transferring a feed rate from an unrelated sample.

Evaluate the accepted blank and the work it needs next. A narrow kerf is useful only when the remaining stock is usable and the finishing allowance covers the measured deviations.

A controlled preparation route

Five Steps from Incoming Block to Accepted Blank

Define the inspection requirements before the first cut, so the trial answers the production question.

  1. Check the stockRecord material grade, dimensions, mass and visible condition. Identify any supplier restrictions and the locating faces.
  2. Plan divisionLay out the required blanks, cut directions, kerf allowance and material reserved for finishing. Include support and unloading access.
  3. Locate & supportConfirm the datum, fixture contact and separated-piece restraint. Check that the workpiece and fixture fit the equipment.
  4. Cut & recordTrack the actual settings, cut order, wire condition and any interruption. Preserve the link between the setup and the measured blank.
  5. Inspect & releaseCheck agreed size, face geometry and edge condition. Compare the result with the remaining finishing allowance before transfer.

Define what good means

Inspect the Features That Matter Downstream

A blank can be within a size limit and still have unsuitable geometry for its next operation. Identify the datum, measurement method and acceptance criteria for each feature.

特徴What to checkWhy it matters
Size & variationMeasure agreed positions on width, height and length; record each reading.Establish whether the blank contains the stock required for finishing.
Face flatness点検中の面をどのように支持し、サンプリングするかについて合意する。.位置決めまたは加工基準面としての適合性を確認する。.
直角度と平行度指定された基準に対して面の関係を確認する。.後続の加工に角度誤差やテーパーを伝達しないようにする。.
Edge condition入口、出口、支持されたエッジを点検し、許容できないチッピングや亀裂を記録する。.使用可能な材料と、クリアランスを消費する損傷を区別する。.
仕上げ代各面の残りの材料と測定された偏差、および次の加工を比較する。.ブランクが必要なサイズを失うことなく仕上げられるかどうかを確認する。.

図面からフィーチャー固有の受け入れ基準について合意する。トライアルで記録された測定値は、保証された生産公差ではない。公差計画については、を参照のこと。 高精度グラファイト切断.

文書化されたグラファイトトライアル

500 mm棒1本。6回のカット。記録された測定値。.

グレード2554の等方性黒鉛トライアルで、Vimfun SVI250-80で公称500 × 87 × 70 mmの棒が生成された。ワイヤ径補正はオフだった。記録には、幅の変動とその他の結果が含まれている。.

報告されたセットアップでは、0.8 mmワイヤ、50 m/sのワイヤ速度、160 Nの張力、42 mm/minの送り速度が使用された。6回のカットは合計45分かかった。これらはその実行からの条件であり、一般的な操作推奨事項ではない。.

完全なトライアルと測定値を見る
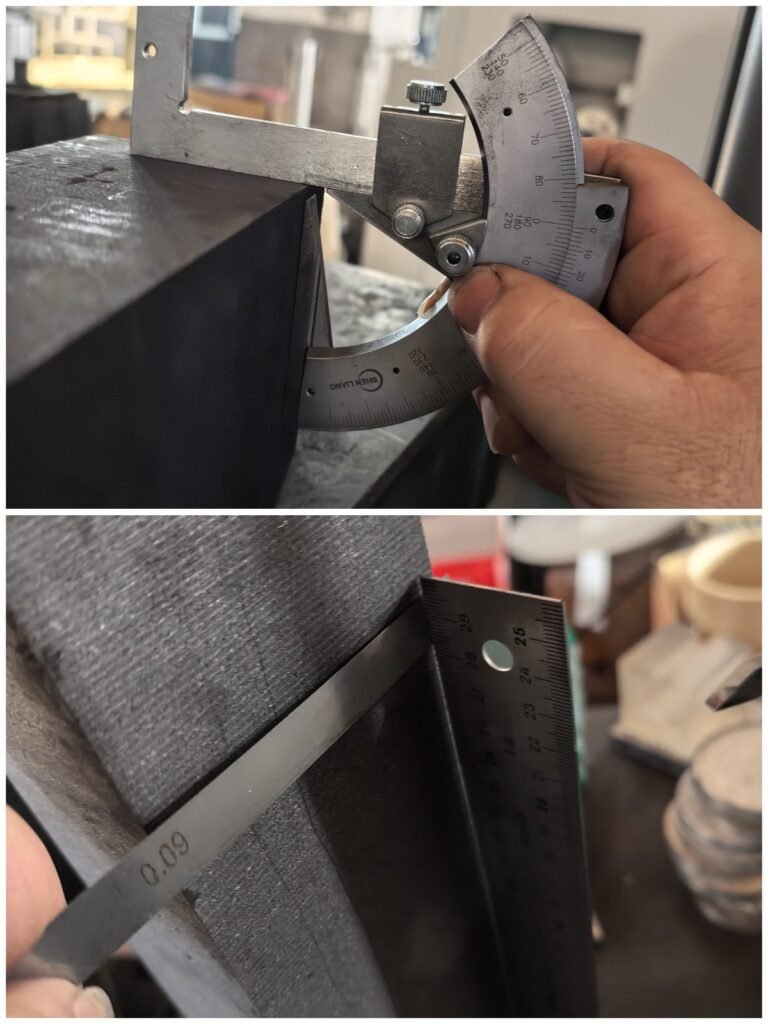
ワイヤーカットグラファイトバーをチェックするスクエアとシックネスゲージ
同じ文書化されたトライアルからのショップフロアでの直角度点検。.
記録されたチェック報告された測定値解釈
幅・公称87 mm00–87.30 mm幅は棒に沿って増加した。仕上げ代を決定する際に結果をレビューする必要がある。.
厚さ・公称70 mm90–70.10 mmこのサンプルとセットアップの記録であり、普遍的な公差ではない。.
直角度ギャップ09–0.15 mm直角度/シックネスゲージのギャップ測定値。角度測定ではない。.
面インジケータ測定値01–0.03 mm500 mmの面1つに対する6回のショップフロア測定値。表面粗さの完全な測定証明ではない。.

トライアル境界: 棒1本、実行1回、手持ち測定器、補正オフ、表面粗さ測定なし。詳細な記録を使用して、独自の受け入れトライアルを計画してください。.

加工ワークピースの周りを選択

容量、ハンドリング、切断ルートを指定する

ワークピースと治具エンベロープを一緒に確認する。機械の移動だけでは、ロードアクセス、サポート、または必要なすべての面を生成する能力を確立できない。.

選択入力提供する情報選択結果
材料エンベロープと質量最大のブロック寸法、重量、ハンドリングアクセス、治具スペース。.作業エリア、テーブル容量、ロード配置を確認する必要がある。.
切断方向とブランクジオメトリ切断レイアウト、再配向シーケンス、ターゲットブランクサイズ。.垂直または水平ルートと必要なサポートおよびアクセスを比較する。.
品質とクリアランス必要な面の関係、サイズ制限、最終加工用の材料。.代表的なトライアルと測定計画を定義する。.
生産需要バッチあたりのブランク数、材料変更、予想される中断。.セットアップ時間、検査、および許容される生産量を能力評価に含めます。.

仕様については、個々の装置ページを参照してください。構成を選択する前に、材料と治具への適合性を確認してください。.

プロセスレビューを継続する

関連する切断トピックを探る

実践的な質問

切断プロセスを指定する前に

切断されたブランクは直接生産に使用できますか?

それは図面と意図された用途によります。サイズ、形状、エッジの状態、および表面の要件を確認してください。多くのブランクは、依然としてフライス加工、穴あけ加工、研削加工、またはその他の仕上げ加工が必要です。.

どのくらいの仕上げアロワンスを残すべきですか?

要求される仕上げ形状、測定された切断偏差、位置決め方法、および後続の操作からアロワンスを設定します。代表的な在庫で試行して確認してください。すべてのグラファイトブロックに適合する単一のアロワンスはありません。.

試行設定を異なるグラファイトグレードに使用できますか?

それらはそのテストの記録として使用してください。材料グレード、切断セクション、治具、ワイヤーの状態、および装置は、作業可能なプロセスウィンドウを変更する可能性があります。異なる用途には、独自の認定が必要です。.

縦型切断と横型切断のどちらを選択すべきですか?

実際の切断レイアウト、サポート、ロードアクセス、および必要な再配置を比較してください。方向だけでは、最適な生産ルートは確立されません。.

切断試行に必要な情報は?

グラファイトグレード、入荷在庫サイズと質量、ターゲットブランク図面、許容基準、仕上げアロワンス、および期待されるバッチ量を提供してください。後続の操作と、試行で解決すべき問題を含めてください。.

実際のワークピースから始める

グラファイトブロック切断試行の計画

在庫とターゲットブランクの要件をお送りください。切断ルート、装置の適合性、および結果を評価するために必要な測定値を確認できます。.

要件を送信する

含めるもの

  • グラファイトグレードと入荷ブロック寸法
  • 加工ワークピース質量とターゲットブランク図面
  • サイズ、形状、およびエッジの許容基準
  • 仕上げアロワンスと後続の操作
  • バッチ数量と期待される生産率

利用可能な場合は、図面またはサンプルの写真を含めてください。.

トップに戻る