グラファイトブロック切断歩留まりは、より多くの入荷材料が所定の納期条件を満たすブランクとして受け入れられるようになると向上します。より狭いカーフ幅は役立ちますが、過度の修正が必要なブランクや仕上げができないブランクを補うことはできません。.
機械を比較する前に、材料収支を立ててください。オペレーションに入ってくるもの、受け入れられた出力として出ていくもの、回収可能な材料として残るものを明記してください。その境界線がなければ、2つの魅力的な歩留まり率は異なるものを表す可能性があります。.
の industrial graphite block cutting page 材料準備を対象としています。この記事は、一般的な事業収益性や下流のプレート歩留まりではなく、初期分割時の材料会計に焦点を当てています。.
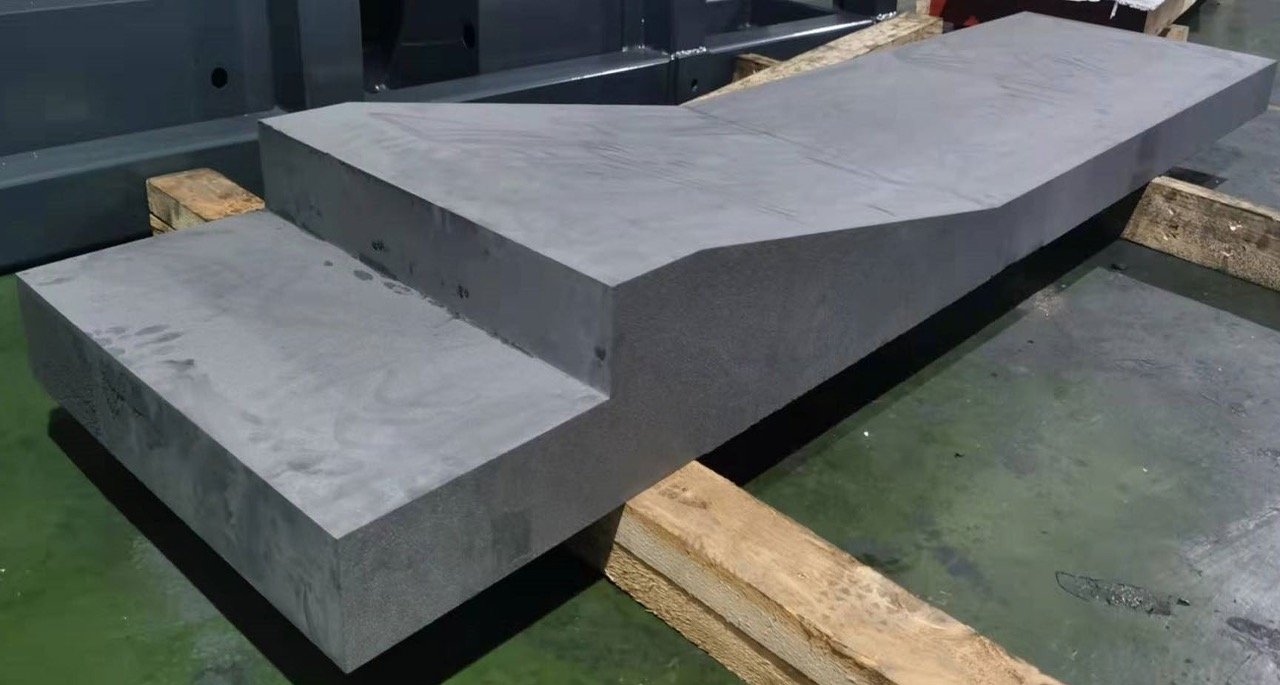
グラファイトブロック切断歩留まりの境界を定義する
一貫した基準を選択してください:体積、質量、または同等ブランクの数。受け入れられた出力が、切断済みブランクまたは完成部品を意味するかどうかを記録してください。体積ベースのブランク回収率と、数ベースの完成部品歩留まりを比較しないでください。.
質量を使用する場合は、材料と測定基準を特定してください。体積を使用する場合は、体積を計算するために使用した寸法を定義してください。公称の材料エンベロープは、損傷した角や不規則な表面の周りに残る実際の材料を表さない場合があります。.
ジョブを比較する際に、グレードの同一性を維持してください。. SGL Carbon は、その等方性グラファイトグレードを区別しています。. 幾何学的な比較を、関連するグレードと購入基準を確認せずに材料コストの主張に翻訳しないでください。.
回収可能な残材を受け入れられたブランクとは別に保管してください。有用な残材は将来的な価値を持つ可能性がありますが、定義された用途と受け入れ条件を満たすまで、現在の注文出力にはなりません。.
材料損失を有用なカテゴリに分類する
カーフ、計画トリム、機械加工代、使用不可能な残材、および拒否されたブランクを個別に記録してください。これらのカテゴリは、異なる是正措置につながります。切断幅を狭めても、誤った基準関係で拒否されたブランクの問題は解決しません。.
Allowance deserves particular care. Material reserved for finishing is part of the as-cut blank, not kerf loss. When assessing finished-part recovery, the portion later removed belongs to a downstream operation.
Do not count a whole rectangular bounding box as recovered material if only an irregular portion is usable. Likewise, do not discard every small remnant automatically. Define the dimensions, condition and storage rules that make an offcut reusable in your operation.
For graphite block cutting yield, use the categories to explain the result, not just to produce a favorable total. A meaningful improvement can then be linked to a change in layout, cut count, allowance or acceptance.
A Clearly Labeled Layout Calculation
Consider an illustrative one-dimensional division problem, not a Vimfun test. A 500 mm stock dimension is to supply 70 mm blanks. Assume seven blanks and six separating kerfs, each 0.8 mm wide, with no end trim for this simplified calculation.
Required length is `7 × 70 + 6 × 0.8 = 494.8 mm`, leaving 5.2 mm in that direction. Blank length allocation is 490 mm. The calculation says the nominal arrangement fits; it says nothing about real cut accuracy or whether the remainder is useful.
Now assume 1 mm of finishing stock on each side along that dimension. Each blank becomes 72 mm before finishing. The same arrangement would require `7 × 72 + 6 × 0.8 = 508.8 mm`, so it no longer fits in 500 mm.
| Illustrative condition | Required stock length | Outcome |
|---|---|---|
| Seven 70 mm blanks; six assumed 0.8 mm kerfs | 494.8 mm | Nominally fits before other allowances |
| Seven 72 mm blanks; same assumed kerfs | 508.8 mm | Does not fit |
| Real production layout | Requires measured inputs | Check trim, geometry and acceptance |
Here 0.8 mm is an assumed kerf for arithmetic. Wire diameter is not automatically the measured kerf. Keep that distinction explicit when replacing assumptions with trial data.
Improve Graphite Block Cutting Yield Through the Layout
Start by mapping required blank sizes and orientation constraints. Consider whether a different division order produces usable remnants rather than narrow scrap. Review the support and handling consequences before accepting a denser layout.
Avoid using nominal cut positions without checking their tolerance and the actual stock envelope. A layout that fits exactly on paper can fail once edge trim, locating stock or a required cleanup pass is included.
Reduce unnecessary cuts where the geometry allows, but compare the resulting blank condition. A saved pass can create a less useful reference or a difficult remaining section. Keep production practicality in the same review as recovery.
使用 low-kerf graphite cutting guide for cut-width economics. The block-specific decision here is whether the complete initial layout produces accepted blanks and usable remnants.
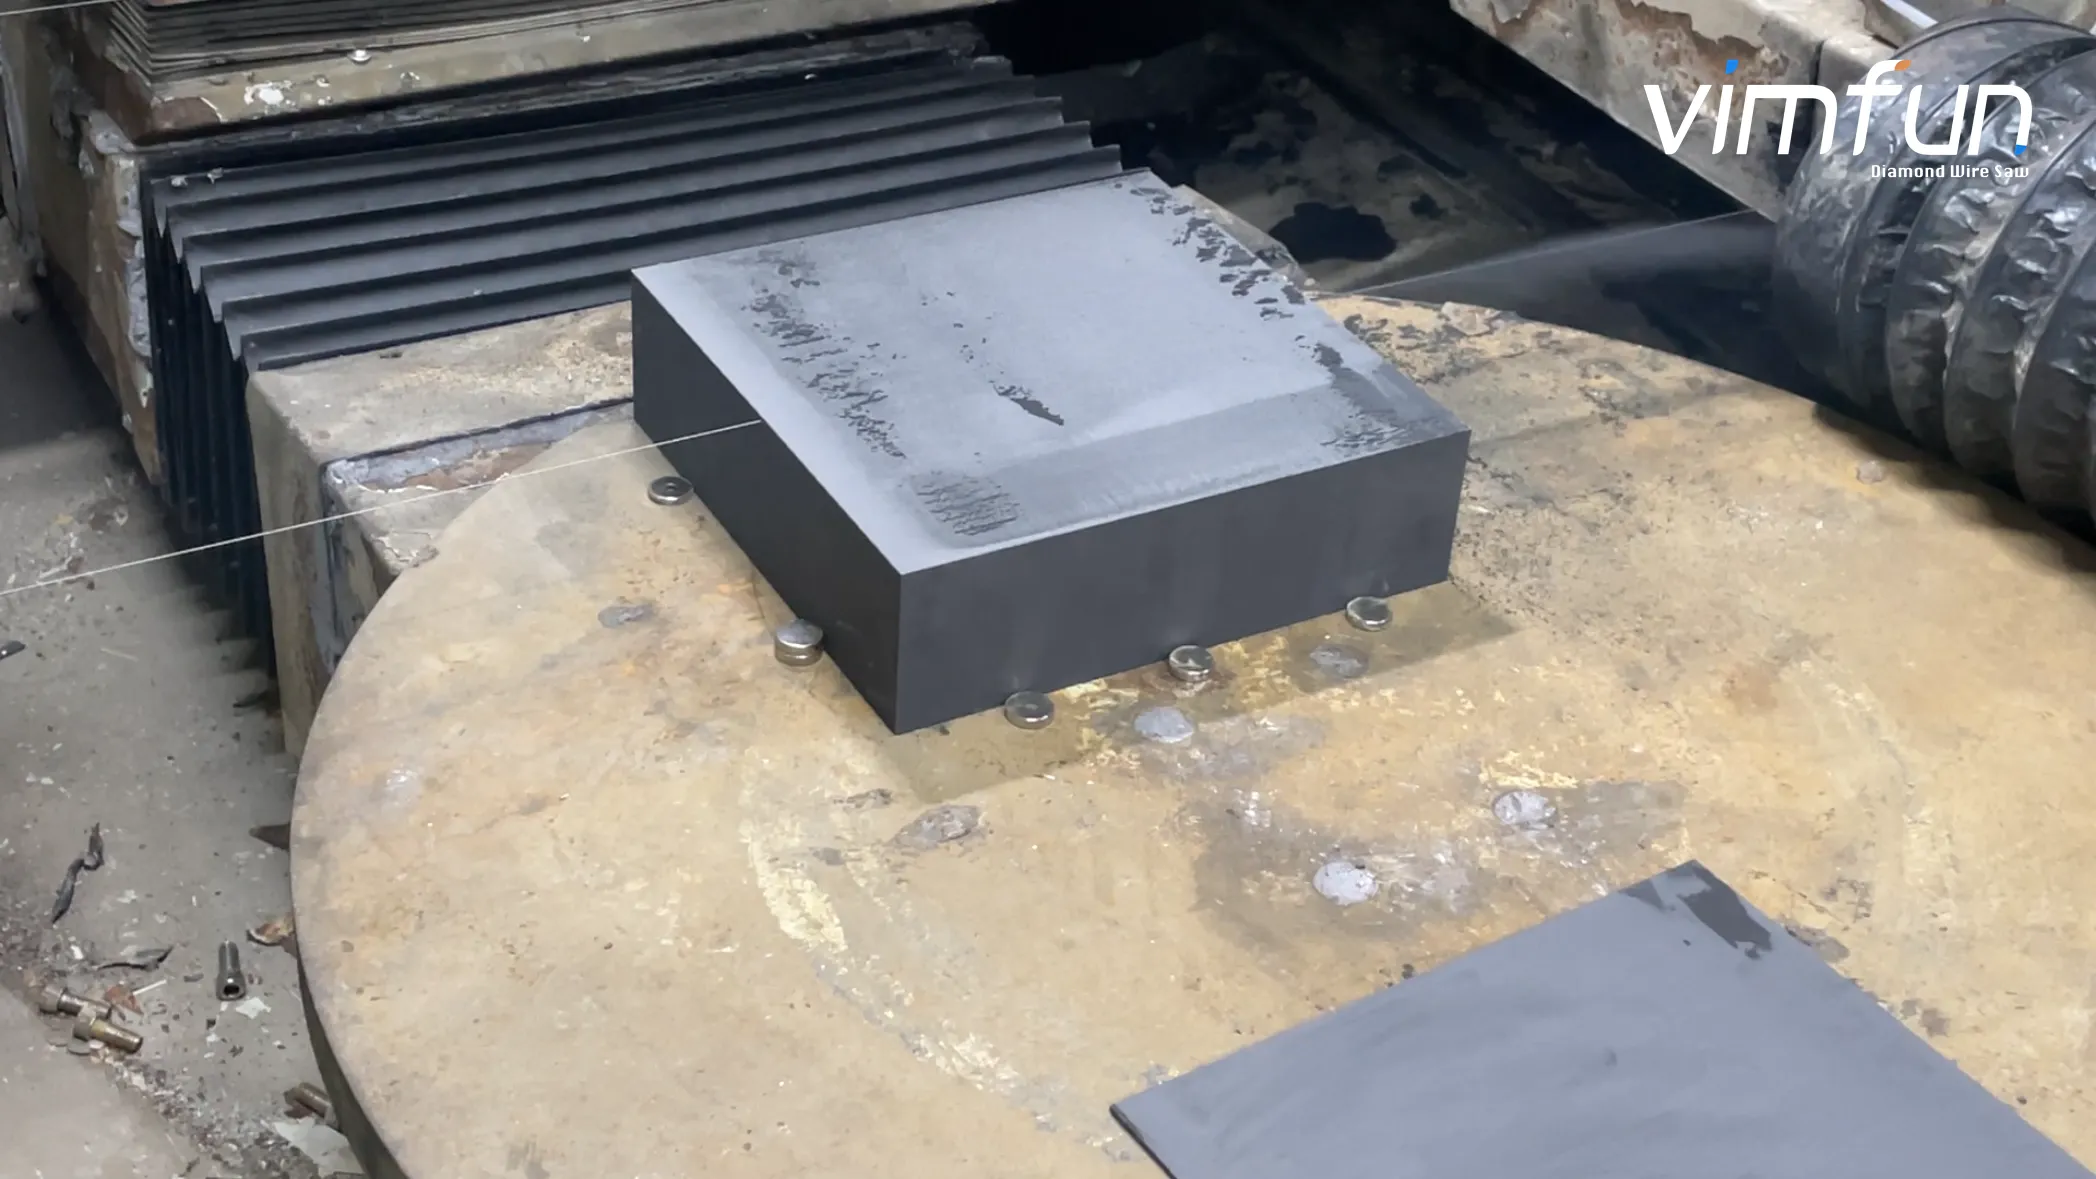
Video: Stock division and handling context
Watch on YouTube · Vimfun Endless Diamond Wire Saw
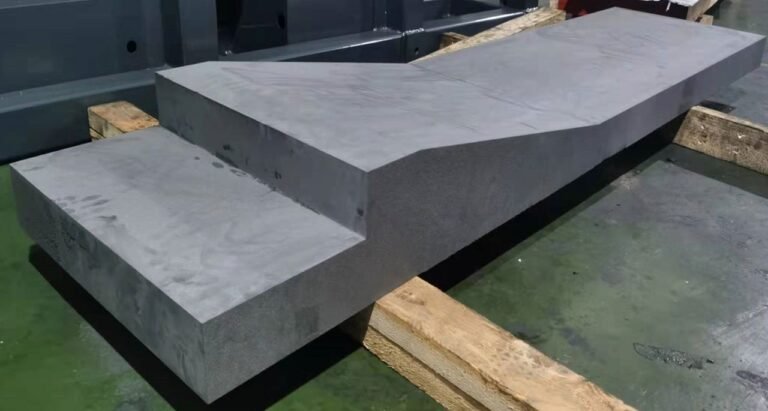
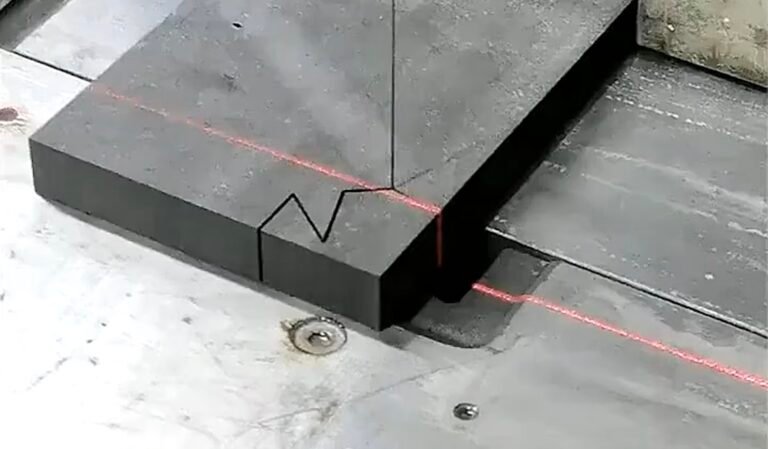
The equipment and block-cutting views illustrate the stock-division stage. No recovery percentage can be calculated without the original stock, accepted blanks and remaining-material records.
Field Notes: Geometry Can Consume the Expected Saving
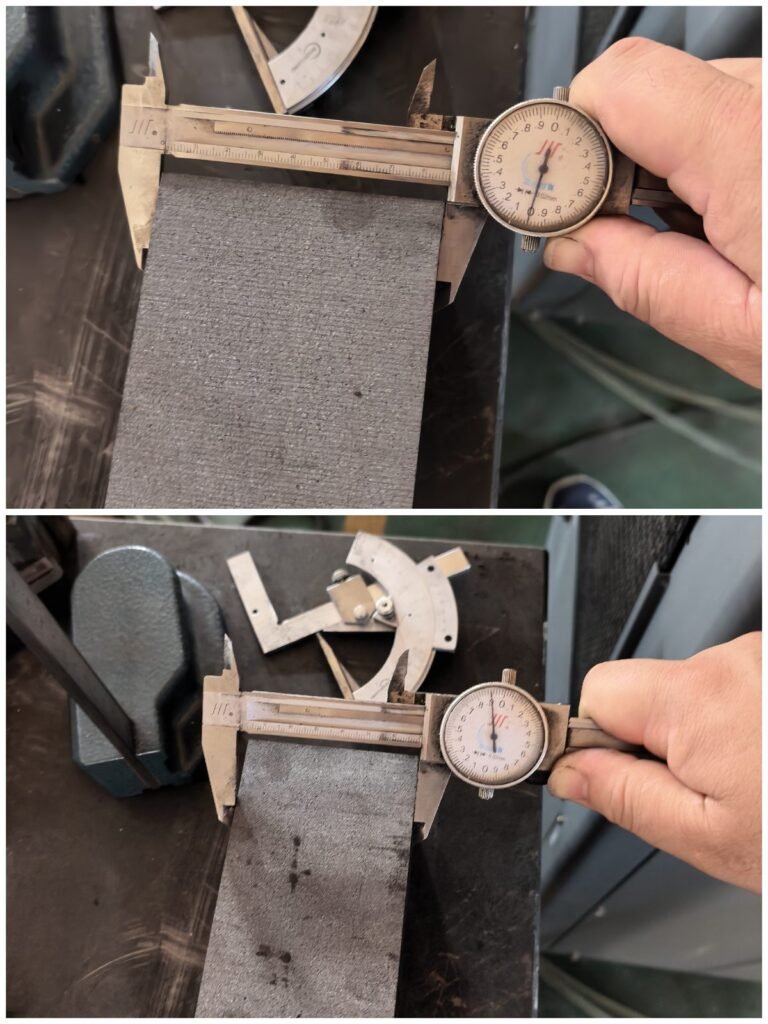
の中で documented SVI250-80 trial, one nominal 500 × 87 × 70 mm grade 2554 bar was cut with compensation off. Width increased from 87.00 to 87.30 mm, while thickness ranged from 69.90 to 70.10 mm.
The run used 0.8 mm wire, but the record does not establish that every kerf was exactly 0.8 mm wide. It also does not report a complete incoming-block material balance or accepted-blank recovery percentage.
The useful shortcoming is the measured width taper. Any later correction must be considered when deciding how much material is actually delivered for finishing. A headline wire diameter cannot represent that entire outcome.
Do not derive a graphite block cutting yield percentage from the sample’s nominal dimensions alone. The necessary input stock volume, all cut losses and the acceptance boundary are not fully specified for that purpose.
Measure Recovery Without Hiding Rejection
Use an order-level ledger that follows material through initial division. Identify each blank and remnant, its dimensions or mass, acceptance status and disposition. Retain the reason for rejection rather than putting every loss into a single scrap category.
Include the method used to measure the material balance. NIST’s uncertainty guidance explains why measurement quality affects decisions. Apply that narrowly: know whether apparent recovery differences exceed the limitations of your dimensional or weighing method.
Compare like orders or clearly identify the differences. A change in blank size, material grade or remnant policy can improve the reported recovery without changing the cutting performance.
の material utilization guide addresses the wider accounting framework. Keep the initial block stage identifiable so its losses are not confused with later profiling or finishing.
Turn the Ledger into a Corrective Action
If kerf dominates, investigate measured cut width and cut count under comparable conditions. If trim dominates, review incoming stock and datum preparation. If rejected blanks dominate, inspect the defect and acceptance requirements before redesigning the layout.
When allowance dominates final loss, review why it is needed. A smaller allowance is useful only if the cutting and locating route can consistently preserve the final geometry. Do not simply remove stock from the drawing to improve the spreadsheet.
Track the next operation’s feedback. A blank accepted at initial division may still consume unexpected stock during finishing. Keep that information separate but linked, so graphite block cutting yield improvements do not create a downstream loss.
Known Limitations / Trade-offs
A denser layout can reduce geometric waste while complicating support and handling. A usable remnant can also require identification and storage that outweigh its practical value for a particular operation.
The arithmetic example is deliberately simplified. Real layouts need cut orientation, edge trim, fixture requirements and measured geometry. It provides no demonstrated production yield or machine performance figure.
Material recovery alone does not establish delivered-part cost. Include setup, inspection, finishing and accepted production where those affect the buying decision. A lower scrap volume can coexist with a more expensive route.
Build a Reusable Material Ledger
Assign each incoming block a traceable job reference and keep the planned division drawing with its actual output. List accepted blanks, retained remnants, planned trim and rejected material as separate records. Where dimensions rather than mass are used, state the geometry assumed in each calculation.
Reconcile the categories before comparing jobs. An unexplained remainder may be a measurement limitation, an omitted trim operation or a classification error. Investigate it instead of silently assigning it to useful recovery.
Carry the receiving operation’s feedback into a linked record. Keep initial blank recovery separate from final-part recovery, but preserve the relationship so an upstream improvement can be evaluated against later correction work.
When reporting graphite block cutting yield, state whether the layout and allowance changed. That gives the reader a reason for the result and makes the calculation useful for future orders with different blank sizes. It also prevents a favorable change in accounting from being mistaken for a demonstrated machine improvement.
Questions for a Yield Review
Is a small wire diameter enough to predict recovery?
No. Measure the relevant kerf and include cut count, trim, allowance, remnants and rejection. Diameter is one process input, not the complete material balance.
Should reusable offcuts be counted as production?
Report them separately unless they meet a defined current-order requirement. State the reuse criteria so a change in accounting does not appear as an equipment improvement.
What information is needed for a layout proposal?
Incoming stock dimensions, required blanks, material grade, orientation constraints, allowances, acceptance limits and expected quantities. Include the existing loss categories so the graphite block cutting yield review targets the actual waste.
Send those details through our block-cutting contact page. A marked layout and the receiving operation’s requirements are more useful than a recovery target alone.