고정밀 흑연 절단: 실제 달성 가능한 공차 수준은 얼마인가?
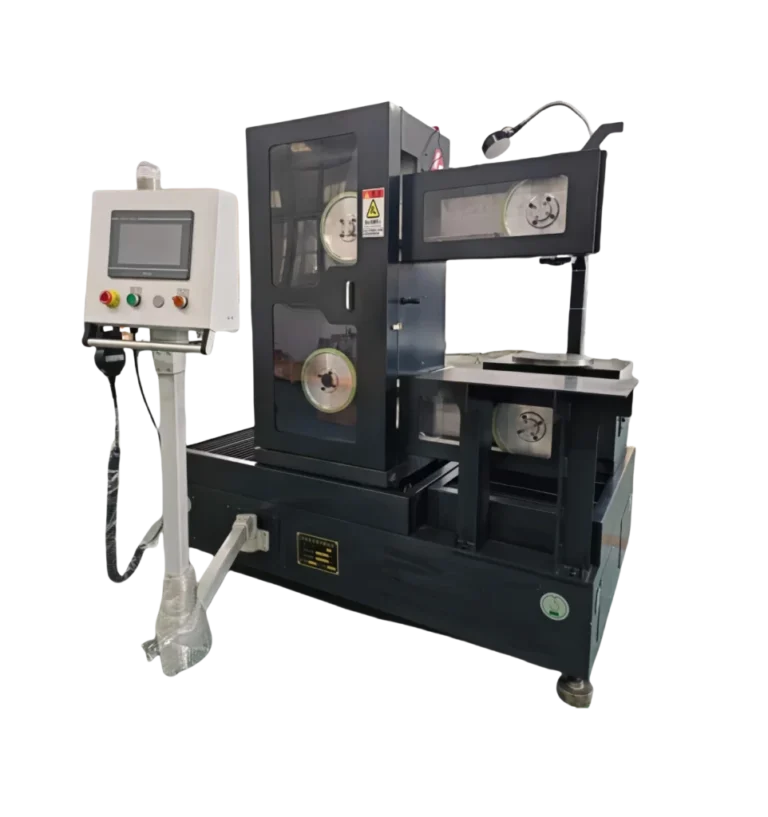
와이어 톱으로 흑연에서 ±0.01mm의 공차를 유지할 수 있다는 말을 들었다면, 데이터를 요청하십시오. 등방성 및 미세 입자 흑연에서 SV60-60 및 SH60-60 기계를 운영한 경험에 따르면, 와이어 톱 절단 시 지속적인 생산 공차는 ±0.03mm이며, 이는 전체 작업 교대 시간 동안 안정적으로 유지되며 모든 것을 일일이 관리할 필요가 없습니다.

와이어 톱으로 흑연에서 ±0.01mm의 공차를 유지할 수 있다는 말을 들었다면, 데이터를 요청하십시오. 등방성 및 미세 입자 흑연에서 SV60-60 및 SH60-60 기계를 운영한 경험에 따르면, 와이어 톱 절단 시 지속적인 생산 공차는 ±0.03mm이며, 이는 전체 작업 교대 시간 동안 안정적으로 유지되며 모든 것을 일일이 관리할 필요가 없습니다.
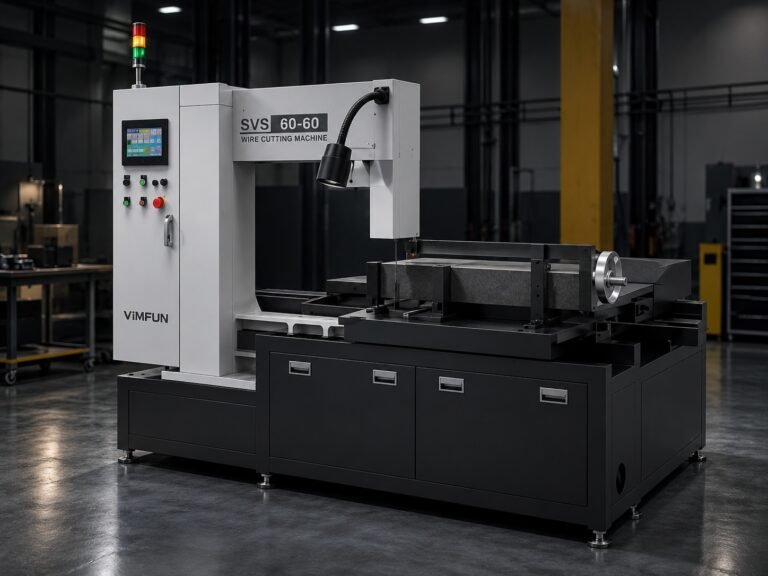
와이어 톱으로 흑연에서 ±0.01mm의 공차를 유지할 수 있다는 말을 들었다면, 데이터를 요청하십시오. 등방성 및 미세 입자 흑연에서 SV60-60 및 SH60-60 기계를 운영한 경험에 따르면, 와이어 톱 절단 시 지속적인 생산 공차는 ±0.03mm이며, 이는 전체 작업 교대 시간 동안 안정적으로 유지되며 모든 것을 일일이 관리할 필요가 없습니다.

A single graphite boat failure in a 12-inch semiconductor diffusion furnace can scrap the entire wafer batch, trigger unplanned line downtime, and force a root-cause investigation that lasts days. Yield loss on that scale is not a materials-quality problem. In a significant share of cases, the failure traces back not
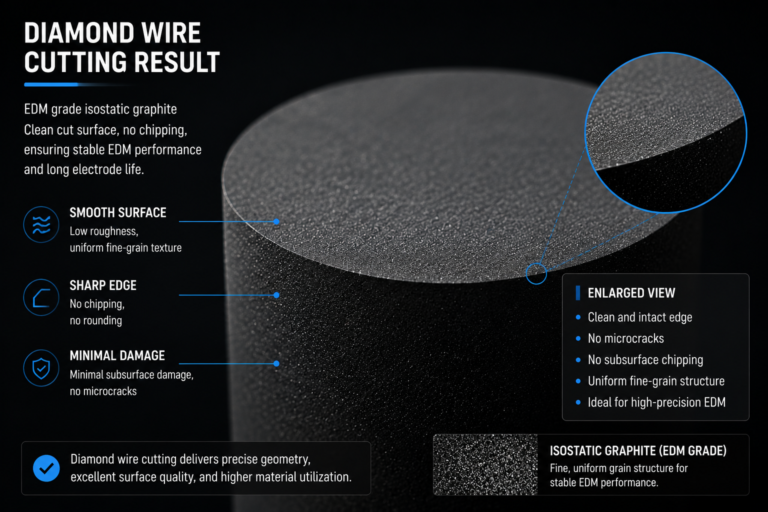
100 mm 절단 길이를 가져와서 명목상 5 mm 조각으로 나눕니다. 1.0 mm의 가정된 절단 폭으로 16개의 완전한 조각이 가능하며, 0.5 mm의 가정된 절단 폭으로는 18개가 가능합니다. 이것은 생산 벤치마크가 아닌 기하학적 예시이지만, 낮은
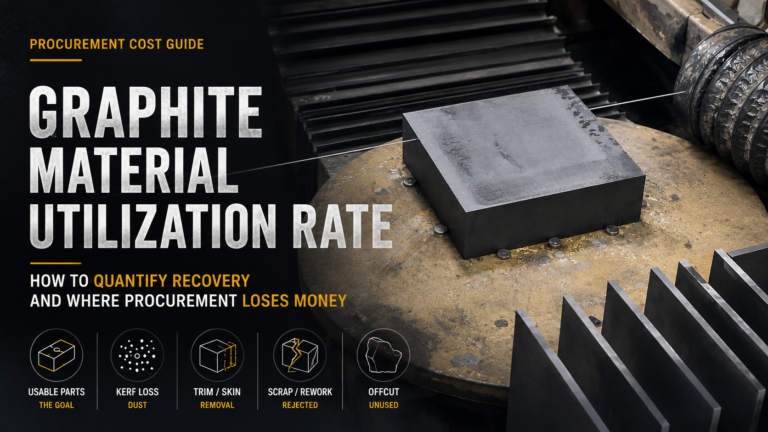
등방성 흑연 블록은 견적, 절단 및 완제품으로 납품됩니다. — 그리고 블록 송장과 완제품 재고 사이 어딘가에서 상당량의 재료가 커프 먼지, 트리밍 및 절단물로 변합니다. 이 간격은 흑연 재료 활용률이며 종종 보이지 않습니다.
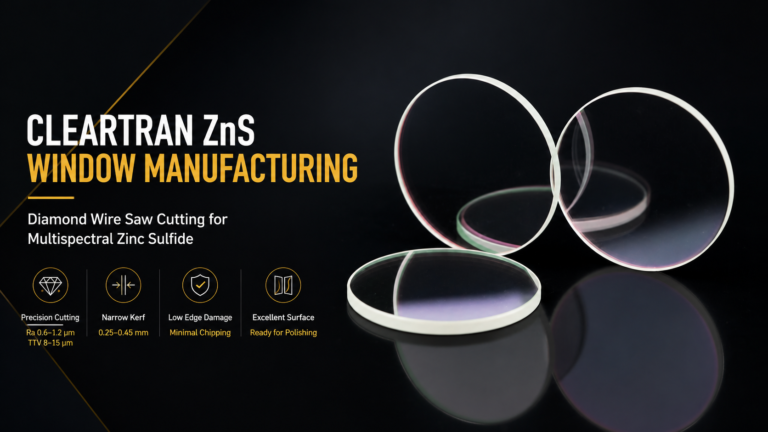
Cleartran ZnS is a denser, tougher grade of zinc sulfide that requires more disciplined cutting control than standard CVD ZnS. Cut it with standard parameters and you get acceptable dimensions but elevated subsurface damage — which shows up later as scatter in the finished window. Cleartran ZnS window manufacturing done
Thin kerf graphite slicing produces narrower cut widths than standard slicing — recovering more material per block while holding tighter dimensional tolerances across the batch. The process works well when parameters are matched to the specific graphite grade and geometry. When they aren’t, the failure modes are fast and difficult
Graphite passes all tests. However, several chips can be harmed. This can happen if it removes faulty trace bits during use. The damage usually appears after shipping. Years of negotiating with graphite suppliers provide that. It’s apparent that semiconductor purchasers hold graphite machining companies to greater standards than other industries.
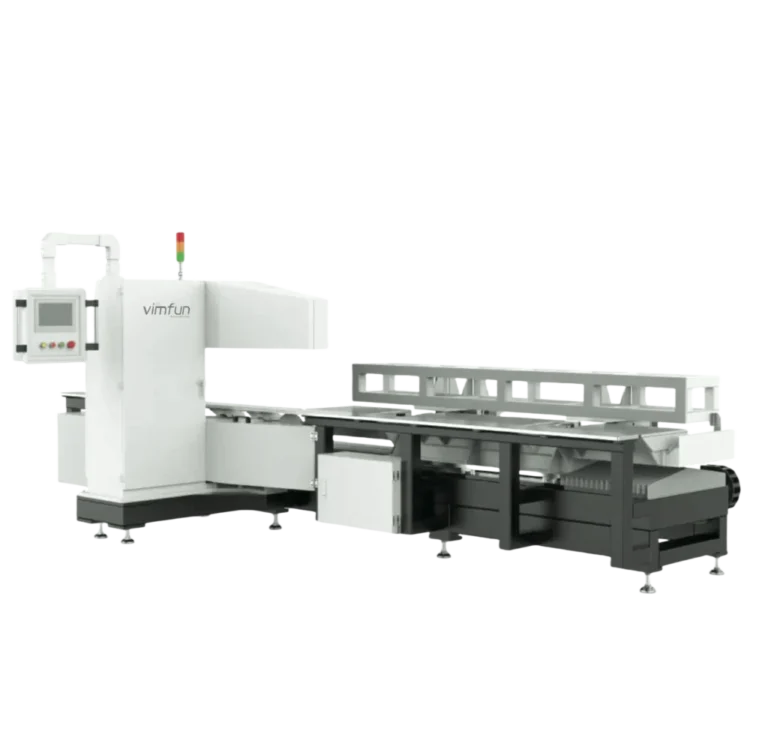
Most cutting machine accidents don’t happen during the cut. These occur when material slides unexpectedly while loading or setting. Vertical cutting machines improve material handling safety, one of three key benefits. Fixture systems secure material while cutting. Second, support structures prevent weight-driven sliding or falling. Third, the control systems adjust
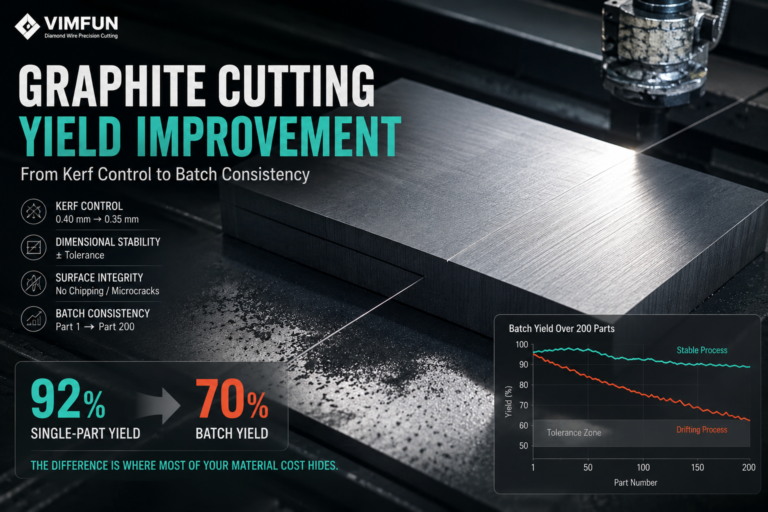
A graphite cutting operation running at 92% single-part yield can easily drop to 70% batch yield across a 200-part production run — the difference is where most of your material cost hides. Graphite cutting yield improvement is not about improving one cut; it is about controlling the variance across every